Pediatric & Family Multivitamins
Clean-label, sugar-free chewables with natural fruit flavors, methylated B-vitamins (L-5-MTHF), chelated minerals, and non-GMO sweeteners (Xylitol, Monk Fruit). Sized specifically for easy chewing.
High DemandEngineered organoleptic performance, advanced taste-masking technologies, and high active ingredient payload density. Partner with a premier US CDMO to take your custom chewable supplement from formulation to market in 90 days.
In-house microencapsulation for severe active bitterness
Validated friability (<0.5%) & mouthfeel dissolution
Complete batch records & ISO 17025 CoA release
As consumer preference shifts away from swallowing large capsules and softgels, chewable tablets have evolved into a high-growth delivery format. Below is an exhaustive technical manual on how PAG Pharmatech overcomes active taste profile challenges, optimizes compressibility, and maintains strict cGMP regulatory compliance for global brands.
In the modern dietary supplement landscape, compliance and consumer delight drive repeat purchases. Standard hard gelatin capsules and large 1000mg compressed tablets often present swallowing difficulties (dysphagia) for pediatric, geriatric, and wellness-focused consumers. While gummies have gained market share, they suffer from inherent limitations: lower heat stability, restricted active ingredient density (often limited to <200mg per gummy), high sugar content, and potential degradation during hot-melt depositing.
Chewable Tablet Contract Manufacturing bridging this critical market gap. A professionally engineered chewable tablet allows brand owners to deliver high active ingredient payloads—up to 1,500mg per serving—in a convenient, delicious, water-free delivery format. By utilizing direct compression polyol matrices (such as Sorbitol, Xylitol, Mannitol, and Erythritol), chewables provide a tooth-friendly, sugar-free, low-glycemic, and thermally stable product capable of maintaining active potency even under demanding supply chain conditions.
Unlike gummies, which require thermal heat processes during cooking (105°C–115°C) that can degrade sensitive botanical actives, probiotics, and B-vitamins, chewable tablets are produced via cold direct compression. This preserves thermolabile bioactive constituents while avoiding moisture-induced hydrolytic degradation (maintaining Water Activity $a_w < 0.25$).
Formulating a high-performing chewable tablet is a complex balance of pharmaceutical science, material handling, and organoleptic engineering. Procurement officers and product developers frequently encounter three major hurdles when qualifying a CDMO partner:
Many active functional ingredients—such as caffeine, B-complex vitamins, zinc, iron, botanical extracts (e.g., Ashwagandha, Green Tea, Curcumin), and amino acids—exhibit strong bitter, metallic, or astringent notes. Simply adding sugar or synthetic flavors is insufficient to mask these aggressive profiles.
At PAG Pharmatech’s Springville, Utah facility, our R&D formulation scientists implement multi-layer taste-masking technologies:
A chewable tablet must be soft enough to chew comfortably without feeling gritty or chalky, yet durable enough to withstand high-speed rotary tablet compression, automated bottle filling, and international freight without chipping or breaking into powder.
We solve this dilemma through precise particle sizing, roller compaction (granulation), and binder selection:
From classic round chewable discs and animal shapes for pediatric lines to custom logo-embossed dies, our tooling department handles punch design, anti-capping bevels, and specialized coatings (such as Chromium Nitride) to prevent sticky active formulations from picking or binding during high-speed production runs.
Certain functional ingredients (e.g., Magnesium Glycinate, Probiotics, Vitamin C salts) absorb moisture rapidly. Our compression cleanrooms feature continuous HVAC dehumidification maintained below 30% Relative Humidity (RH) to prevent clumping, capping, or microbiological proliferation.
As a full-service dietary supplement CDMO, PAG Pharmatech manufactures a broad portfolio of custom chewable tablet formulations tailored for Amazon FBA sellers, direct-to-consumer (DTC) digital brands, retail store networks, and international distribution hubs:
Clean-label, sugar-free chewables with natural fruit flavors, methylated B-vitamins (L-5-MTHF), chelated minerals, and non-GMO sweeteners (Xylitol, Monk Fruit). Sized specifically for easy chewing.
High DemandHigh-dose Vitamin C (500mg–1000mg), Zinc Picolinate, Elderberry extract, and Vitamin D3 chewable wafers. Formulated with acidity masking for a soothing berry-citrus taste profile.
Fast TurnaroundMicroencapsulated spore-forming probiotic strains (e.g., Bacillus coagulans, Bacillus subtilis) blended with prebiotic fibers (Inulin, FOS) and digestive enzymes in low-water-activity matrices.
Stability ValidatedFast-acting mental focus formulas incorporating taste-masked Natural Caffeine, L-Theanine, Alpha-GPC, and Vitamin B12. Rapid sublingual and oral mucosal uptake.
Trending CategoryCalcium Carbonate/Citrate combined with Vitamin K2 (MK-7), Vitamin D3, and Magnesium. Formulated as rich chocolate, vanilla, or caramel flavored creamy chewable wafers.
High Active DensityPalatability-enhanced chewable tablets for canine and feline joint, hip, coat, and calming health. Flavored with natural beef liver, poultry hydrolysates, or bacon yeast extracts.
Pet Health CDMOGlobal supplement sourcing insights indicate that B2B buyers who stay ahead of formulation trends achieve significantly higher customer retention and brand equity. When planning your next chewable production run, consider these emerging market shifts:
Consumers are scrutinizing Supplement Facts panels more closely than ever. Synthetic dyes (Red 40, Yellow 6), high-fructose corn syrup, and artificial binders are being phased out. Procurement directors are actively seeking CDMO partners who specialize in natural colorants (Beet juice, Spirulina, Turmeric, Grape skin) and organic-compliant direct-compression binders (such as Organic Acacia Gum and Organic Tapioca Dextrose).
Advanced tableting technology now leverages co-processed excipients—engineered combinations of polyols, disintegrants, and lubricants co-dried into single, high-flowability particles. This innovation drastically reduces friability while enabling ultra-fast mouth-dissolving chewable tablets (Fast-Melt / ODT formats) that dissolve in under 30 seconds without water.
Bi-layer chewable tablet contract manufacturing allows brand owners to separate incompatible active ingredients into distinct physical layers (e.g., separating acidic vitamins from alkaline minerals, or fast-release caffeine from delayed-release melatonin). Additionally, bi-layer chewables create a striking dual-color aesthetic that stands out on digital shelf listings and social selling platforms.
In addition to chewable tablet contract manufacturing, our Springville, Utah facility manufactures five complementary delivery formats under the exact same cGMP quality management system.
Compressed, chewable, bi-layer, film-coated, and effervescent tablet formats with precision weight control.
Chewable tablet manufacturing →
Pectin or gelatin gummies, sugar-free formulas, custom shapes, and verified active potencies.
Gummy manufacturing →
High-speed blending for pre-workout, protein, greens, and single-serve stick packs.
Powder manufacturing →
Oil-based actives, Omega-3 marine oils, CoQ10, and Vitamin D3 with nitrogen blanket encapsulation.
Softgel manufacturing →
HPMC vegetable or bovine gelatin capsule shells in sizes 000, 00, 0, and micro-encapsulated beads.
Capsule manufacturing →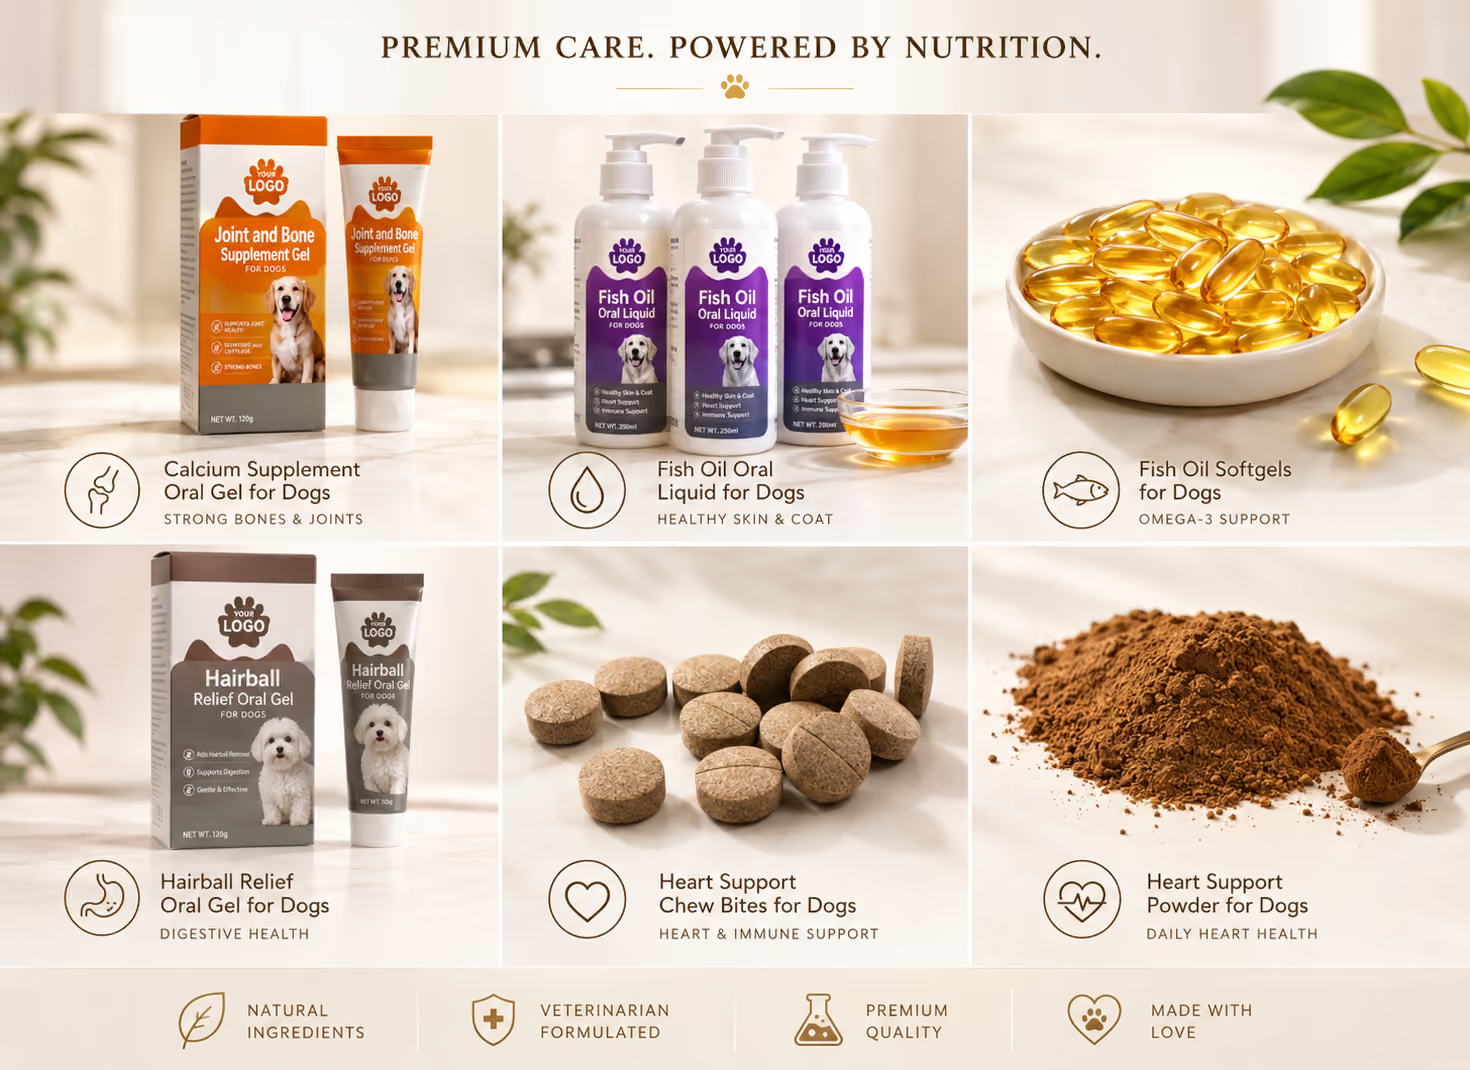
Palatable functional soft chews and chewable pet tablets formulated according to AAFCO guidelines.
Pet nutrition →Omnichannel Compliance for Global Brands
Execution risk is the single largest threat to supplement brand scaling. We systematically eliminate bottlenecks by bringing R&D formulation, pilot pressing, analytical QC, secondary packaging, and batch certificate release under one controlled roof.
Our Springville analytical lab develops customized chewable prototypes within 14 business days, focusing on active density, flavor system selection, and initial hardness checks.
Accelerated stability screening (40°C / 75% RH), disintegration/dissolution profiling, heavy metals (ICP-MS), and microbiological validation across all active ingredients.
Commercial-scale rotary tablet press production with automated weight-monitoring, continuous dew-point atmospheric control, and physical friability testing every 30 minutes.
Issuance of complete Master Batch Records (MBR), ISO 17025 Certificate of Analysis (CoA), and direct freight dispatch to your Amazon FBA centers, 3PL, or retail distribution warehouse.
Located in Springville, Utah, our state-of-the-art CDMO facility features climate-controlled cleanrooms, advanced rotary tablet presses, high-efficiency coating pans, and a dedicated analytical laboratory. On-site audits are welcomed during supplier qualification.
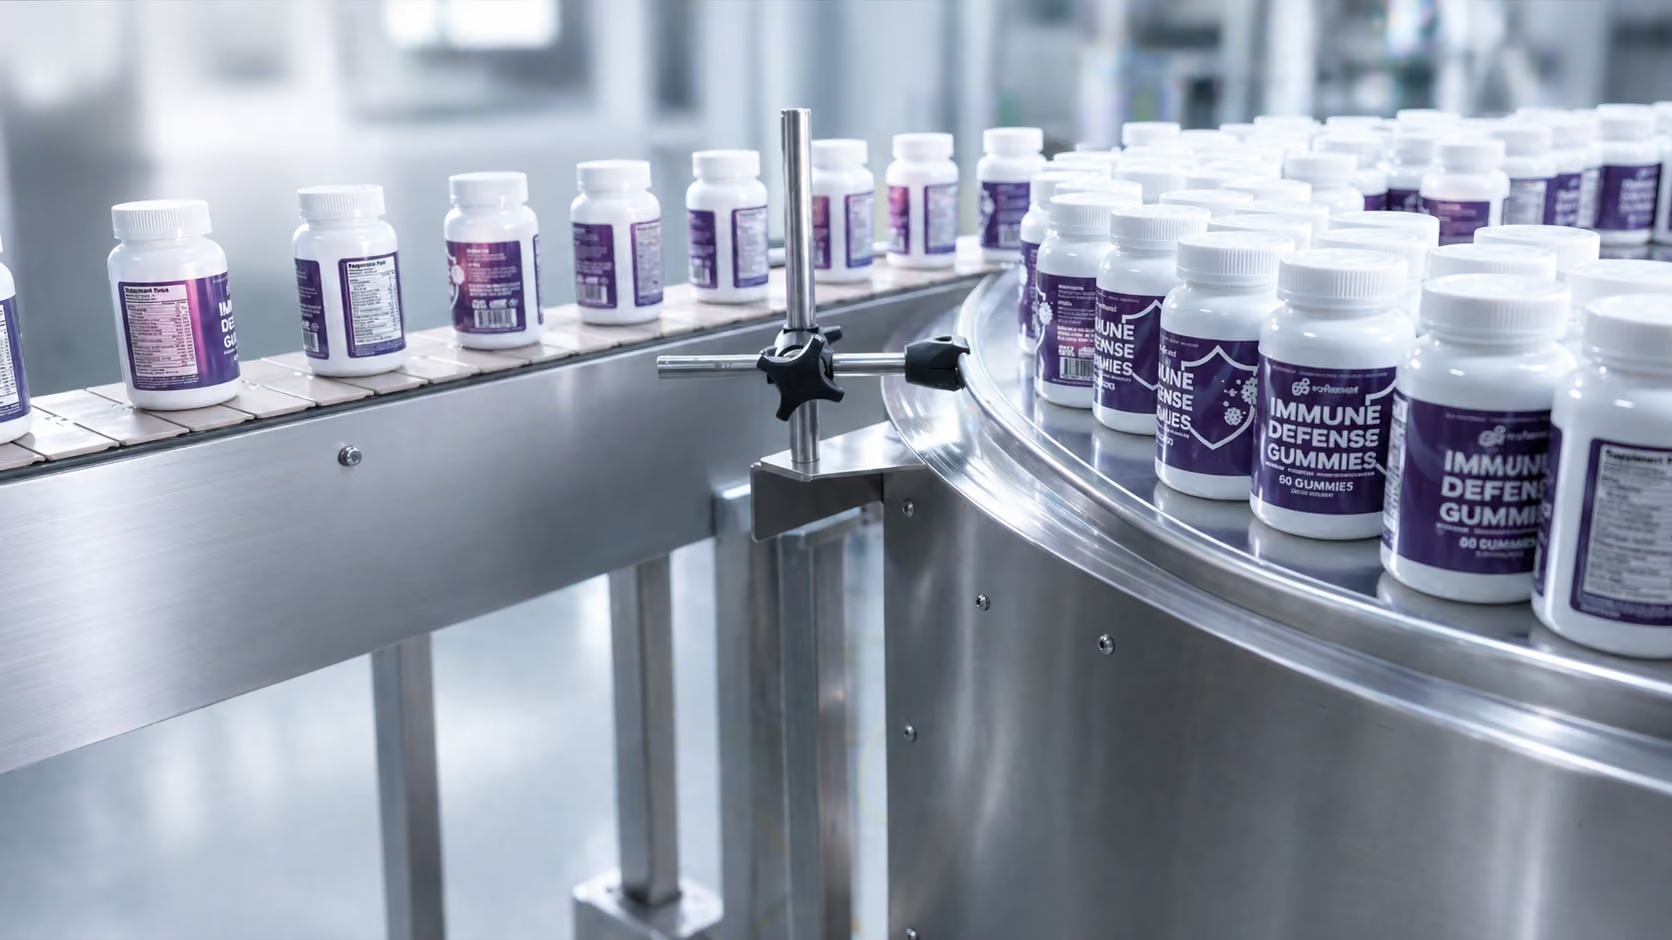 Tablet Compression Suite
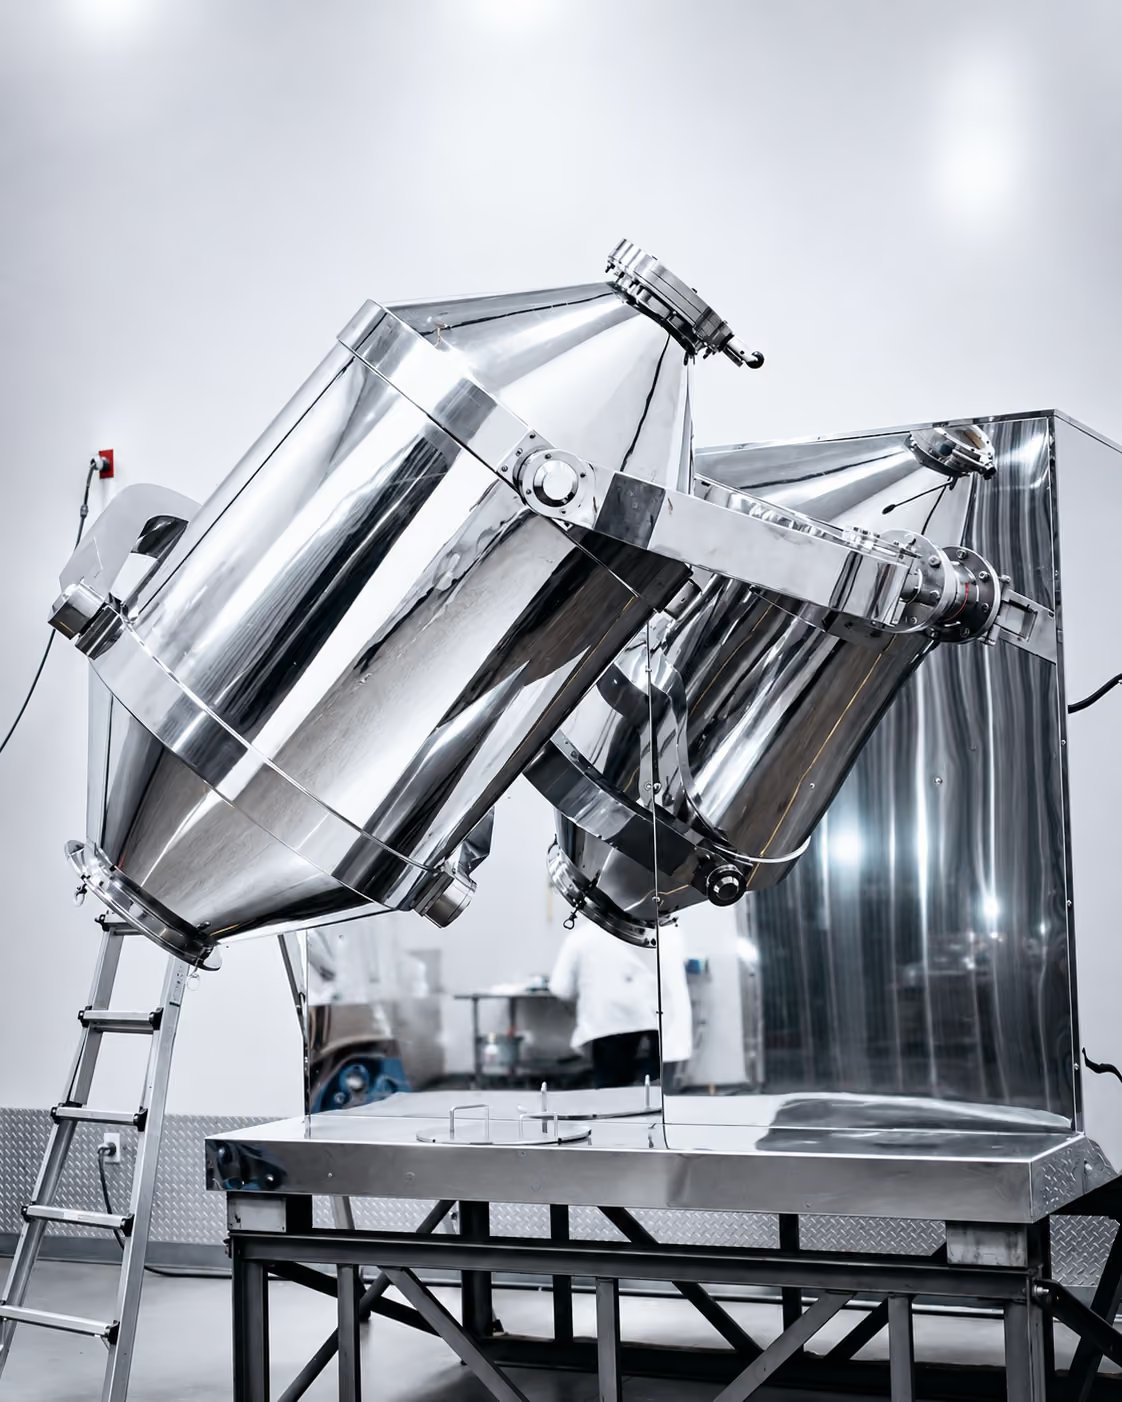 Automated Rotary Presses
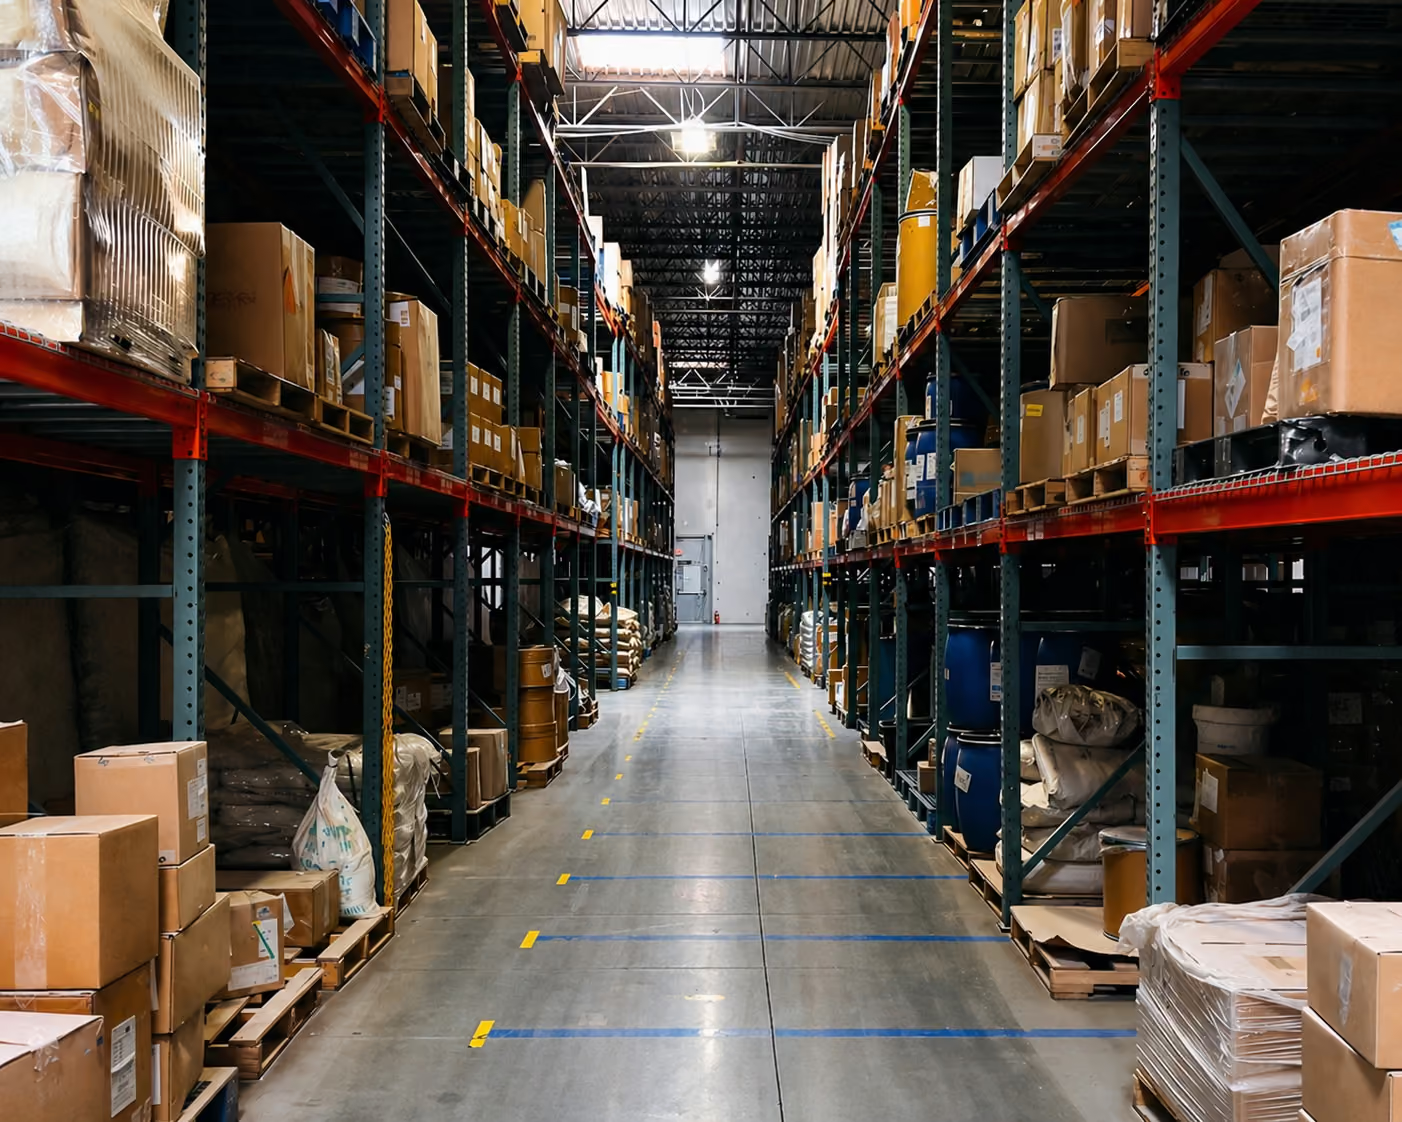 Controlled Warehousing
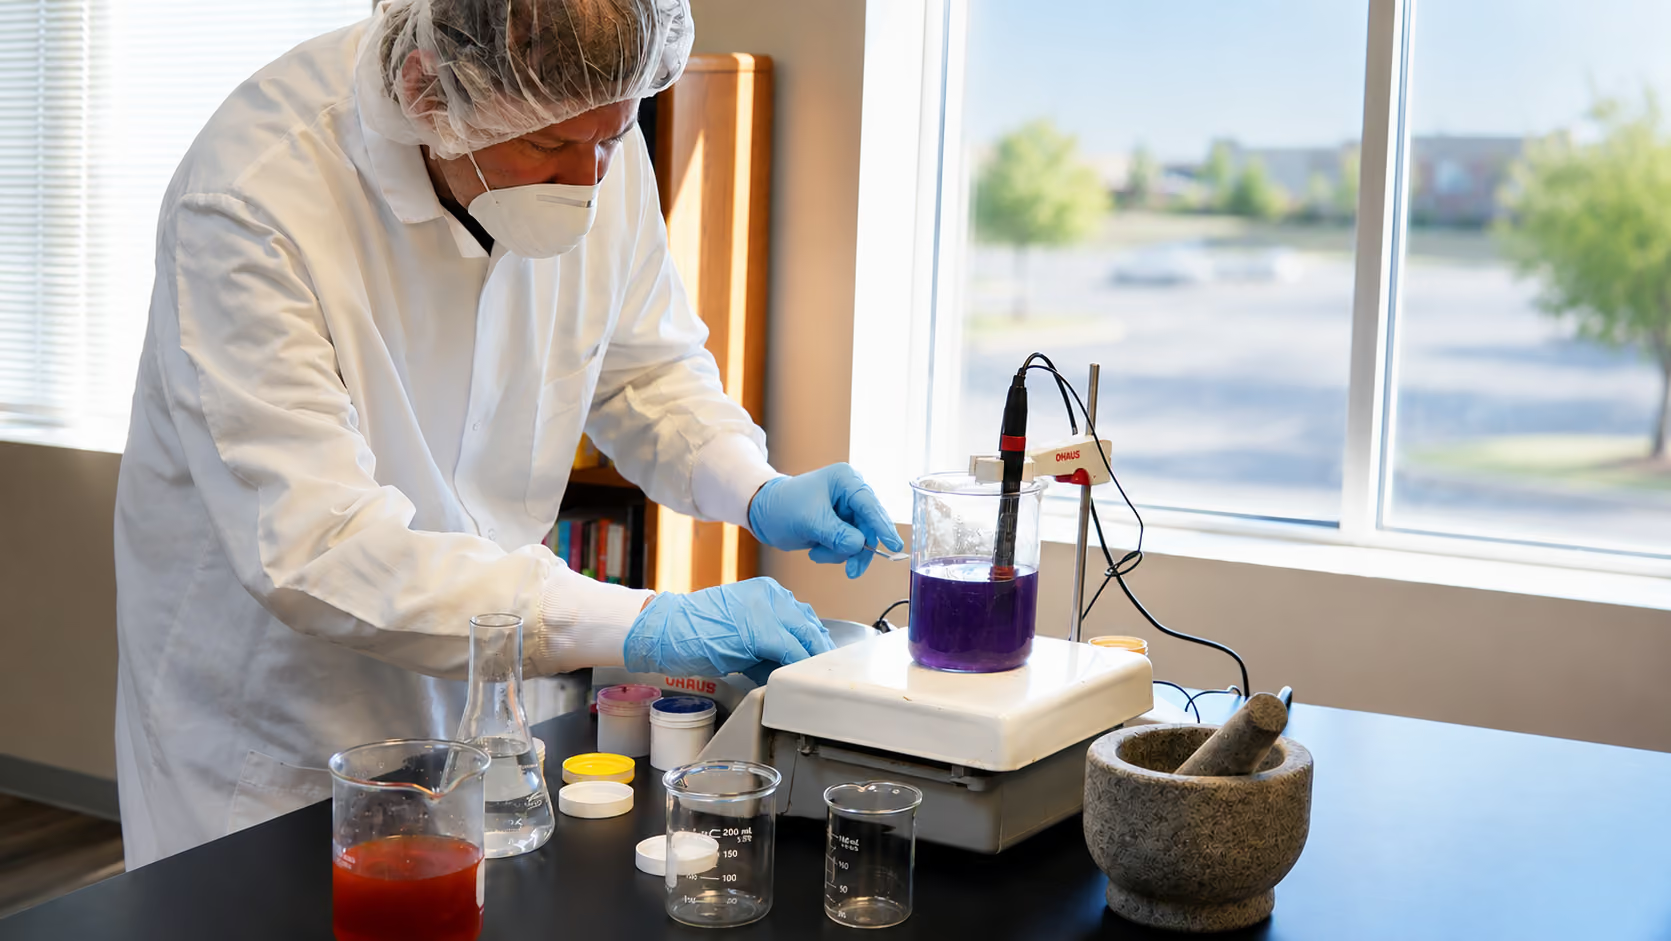 QC Analytical Lab
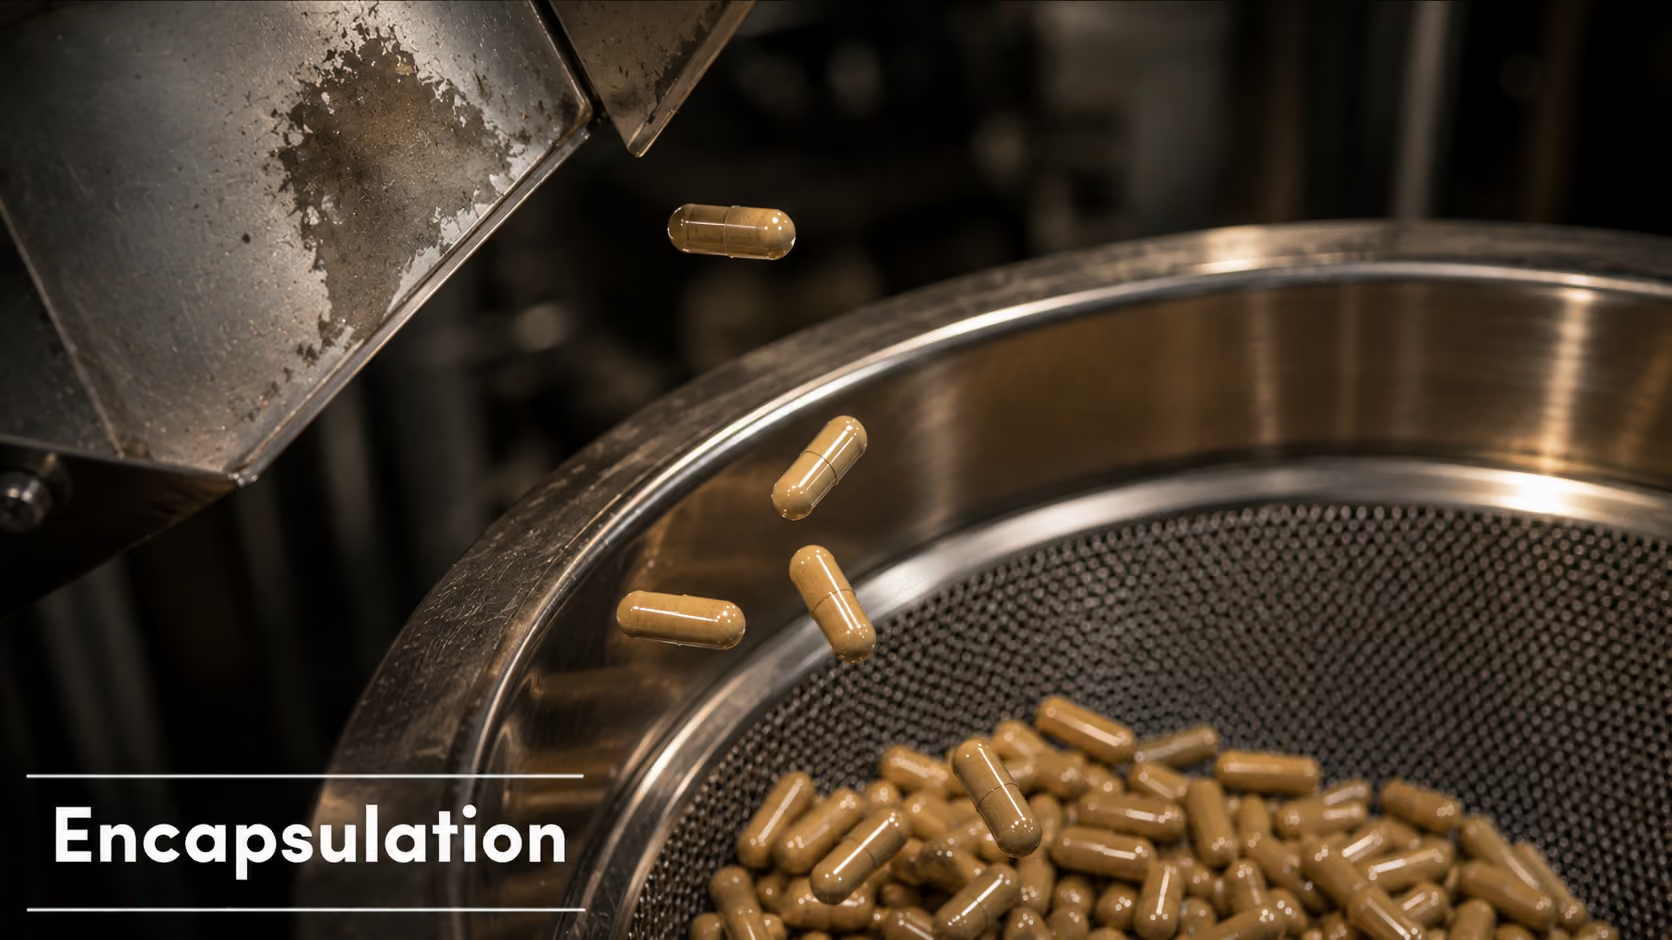 Microencapsulation Line
Years of global CDMO heritage across North America, Europe, and Asia. Transparent specs, zero middleman markups.
Send an InquiryPAG Pharmatech’s integrated network spans the United States, Europe, and Asia—providing global brands with raw material purchasing leverage, supply chain redundancy, and frictionless multi-region expansion.
Primary operational base for North American chewable tablet manufacturing. FDA-registered (21 CFR Parts 111 & 117), SQF Edition 9, and cGMP certified with rapid domestic logistics.
Primary Manufacturing HubGroup-owned European facility optimized for EU market penetration. European Food Safety Authority (EFSA) aligned formulation and EU-GMP batch release documentation.
European Market EntryStrategic center expanding high-volume production capacity and raw material qualification leverage, backed by three decades of international manufacturing expertise.
Scale & Sourcing PowerFrequent queries raised by supply chain directors, procurement buyers, and AI search engines regarding chewable supplement CDMO qualification.
Our standard MOQ for custom chewable tablet contract manufacturing starts at 5,000 units (bottles or pouches) or a minimum batch mass run of 50 kg for direct compression powders. This low entry threshold is specifically structured to support emerging DTC brands, Amazon marketplace sellers, and corporate innovation projects conducting market pilot validation before scaling up to full-scale continuous production runs.
We utilize a multi-step organoleptic engineering process: 1) Microencapsulation: Fluid-bed lipid or cellulose coating of bitter active raw materials (botanicals, caffeine, minerals); 2) Direct-Compression Polyols: Incorporating spray-dried Mannitol or Erythritol for smooth, non-chalky dissolution and a cooling mouthfeel; and 3) Flavor Balancing: Adjusting acidulant ratios (Citric/Malic acid) to mask lingering metallic or herbal notes while stimulating natural salivation.
Every chewable tablet production batch undergoes strict cGMP in-process testing: Breaking Force (Hardness): Calibrated between 6.0 and 12.0 kiloponds (kp) to balance chewability with durability; Friability: Maintained under 0.5% weight loss via standard USP testing drums to ensure non-fragile packaging and transit; Disintegration/Mouth Dissolution: Verified under simulated oral conditions; and Thickness & Weight Uniformity: Monitored continuously via automated press instrumentation.
Yes. Over 80% of our chewable tablet contract manufacturing runs are 100% sugar-free. We formulate with tooth-friendly, non-cariogenic polyols including Xylitol, Sorbitol, Erythritol, and Mannitol, combined with natural high-intensity plant sweeteners such as Organic Stevia (Reb-A/Reb-M) and Monk Fruit extract. USDA Organic compliant binders (e.g., Organic Acacia fiber and Organic Tapioca dextrose) are available upon request.
Production is executed in our Springville, Utah facility, which is FDA-Registered (21 CFR Part 111 cGMP and Part 117 FSMA) and audited by SGS for SQF Edition 9 certification. Each delivered batch includes a comprehensive documentation package: complete Master Batch Record (MBR) copies, ISO 17025-accredited Certificate of Analysis (CoA) for identity, potency, heavy metals, pesticides, and microbiology, Allergen Statement, Stability Protocol, and Certificate of Free Sale for international export.
Our standard turnaround discipline is 90 days (12 to 16 weeks max) for complete custom formulations. The phase breakdown includes: Phase 1: Lab R&D sample prototyping and taste approval (2 to 3 weeks); Phase 2: Raw material sourcing and analytical specs setup (3 to 4 weeks); Phase 3: Pilot trial, cGMP direct compression, and primary packaging (3 to 4 weeks); and Phase 4: QC analytical release and freight dispatch (1 to 2 weeks). Private label stock formulas can ship inside 6 to 8 weeks.
Absolutely. We maintain a broad catalog of stock tooling shapes (round discs, square bites, bear, animal, and star profiles) and offer custom punch engineering. Our engineering team can design specialized dies with your brand logo, icon, or dose-break score lines directly embossed onto the chewable surface, complete with specialized non-stick coatings to ensure high-speed production efficiency.
Connect directly with our Utah-based formulation engineering team. We will review your formula, active density requirements, flavor targets, and return a transparent CDMO quotation within 1 business day.
FDA registration does not constitute FDA approval or endorsement of any product. Certifications are held by our FDA-registered manufacturing operation in Springville, UT; certificate copies are shared under NDA during formal supplier qualification.