US-Based Supplement Manufacturing  ·  FDA-Registered & GMP Certified  ·  8–12 Week Lead Times
FDA Registered SQF Ed. 9 Halal & Kosher 30 Years CDMO
Springville, Utah · FDA-Registered CDMO

Private Label Protein Powder Manufacturing: Technical Specifications, Global Procurement Dynamics, and Formulation Engineering

An end-to-end CDMO blueprint for global brand owners, sourcing directors, and marketplace sellers looking to launch compliant, highly soluble, and commercially scalable protein powder products in under 90 days.

21 CFR 111 & 117 Compliant GMP & SQF Edition 9 ICP-MS Heavy Metal Tested

Protein Powder Manufacturing Metrics

0 kg
Accessible Pilot & Low-MOQ Starting Batch
0 Days
Concept-to-Market Finished Product Release
0.8%
Target Dry Blend Homogeneity (<2% RSD)
0
Global Manufacturing Nodes (USA · EU · CN)

In-house high-shear ribbon and V-blending systems

Automated rigid container & flexible pouch filling lines

Full organoleptic, solubility & assay batch verification

0 kg
Entry-Level Powder MOQ
0 Days
Turnkey Launch Cadence
0%
Batch Identity Verification
0+
Years CDMO Lineage
FDA-Registered USA Production SQF Ed. 9 & cGMP Certified Prop 65 Heavy Metal Verification Global CDMO Network Halal, Kosher & Organic Handling
Executive Sourcing Briefing

Navigating Private Label Protein Powder Manufacturing in Today’s Global Marketplace

Evaluating raw protein substrates, sensory masking chemistry, particle size distribution, and international regulatory compliance for commercial success.

In the modern dietary supplement ecosystem, procurement officers and brand owners face an increasingly sophisticated consumer base. Sourcing a high-yield protein supplement is no longer merely a transaction of purchasing raw Whey Protein Concentrate or isolated Plant Proteins. It demands an end-to-end contract development and manufacturing organization (CDMO) approach that integrates biophysical chemistry, particle engineering, organoleptic stabilization, and rigorous cGMP quality systems.

Whether targeting athletic performance, active aging, body recomposition, or clinical meal replacement, the commercial execution of private label protein powder manufacturing requires strict control over bulk density, hygroscopicity, dispersion kinetics, and heavy metal limits. PAG Pharmatech America operates as a premier Contract Development and Manufacturing Organization (CDMO) out of Springville, Utah, backing every production run with 30 years of global manufacturing heritage, full 21 CFR Part 111 (dietary supplements) and Part 117 (human food) compliance, and SQF Edition 9 accreditation.

Information Gain Insights for B2B Procurement Teams

Unlike standard off-the-shelf catalog blenders, PAG Pharmatech evaluates protein raw materials at the molecular level—measuring Digestible Indispensable Amino Acid Scores (DIAAS), particle size distributions (mesh sizes 60 to 100), and water activity ($a_w < 0.30$) to prevent enzymatic degradation and enzymatic browning (Maillard reaction) during shelf life.
Product Formats & Substrates

Recommended Protein Matrices for Custom Private Labeling

From traditional dairy isolate systems to modern clear plant proteins and collagen hydrolysates, explore the formulation specs engineered at our Utah facility.

Whey Protein Isolate & Concentrate (WPI / WPC)

Engineered using cold-temperature Cross-Flow Microfiltration (CFM) to preserve native native immunoglobulins ($\text{IgG}$) and lactoferrin. Available in WPC 80% and WPI 90% concentrations with instantized sunflower lecithin coating for instant dispersibility without clump formation.

  • Low lactose (<1% for WPI)
  • Complete BCAA profile (~5.5g per serving)
  • Custom instantization protocols

Plant-Based Protein Blends (Vegan / Non-GMO)

Synergistic matrix combining Yellow Pea (80%), Organic Brown Rice (80%), Pumpkin Seed, and Fava Bean proteins. Formulated to achieve a complete amino acid score (PDCAAS = 1.0) while leveraging micro-milling technology to eliminate chalky, gritty mouthfeel.

  • Naturally hypoallergenic & dairy-free
  • Enzymatically debittered substrates
  • Proprietary natural flavor systems

Hydrolyzed Collagen Peptides (Types I & III)

Bovine or Marine derived hydrolyzed collagen peptides optimized to a molecular weight of 2,000–5,000 Daltons for rapid intestinal uptake. Neutral thermal stability allows seamless blending into coffee, beverages, or functional bakery mixes.

  • High hydroxyproline & glycine concentration
  • Cold water soluble without gelling
  • Pasture-raised & grass-fed sourcing

Technical Comparison of Protein Substrates for Private Labeling

  • Post-workout recovery, low-carb formulas
  • Mass gainers, cost-effective daily proteins
  • Vegan protein bases, keto MRPs
  • Complementary blend with Pea Protein
  • Beauty-from-within, joint health, nutricosmetics
  • Juice-style protein drinks, ready-to-mix sachets
  • Protein Substrate Protein Density (%) PDCAAS / DIAAS Solubility Profile Allergen Status Primary Application
    Whey Isolate (CFM) 90% – 92% 1.00 / 1.15 Immediate dispersion; crystal clear solution options Contains Milk (Lactose <0.5%)
    Whey Concentrate (WPC80) 78% – 82% 1.00 / 1.10 High solubility; creamy texture development Contains Milk
    Pea Protein Isolate 80% – 85% 0.89 / 0.82 Moderate; benefits from micronization and blends Allergen-Free (Pea)
    Brown Rice Protein 80% – 90% 0.56 / 0.63 Low-to-moderate solubility; high methionine content Allergen-Free
    Hydrolyzed Collagen 90% – 95% 0.00 (Incomplete) 100% Instant cold-water solubility Bovine / Fish
    Clear Whey / Acid Stable Isolate 88% – 90% 1.00 / 1.14 Transparent in liquid at pH 3.0 – 4.2 Contains Milk
    Manufacturing Capabilities

    State-of-the-Art Powder Blending & Packaging Infrastructure

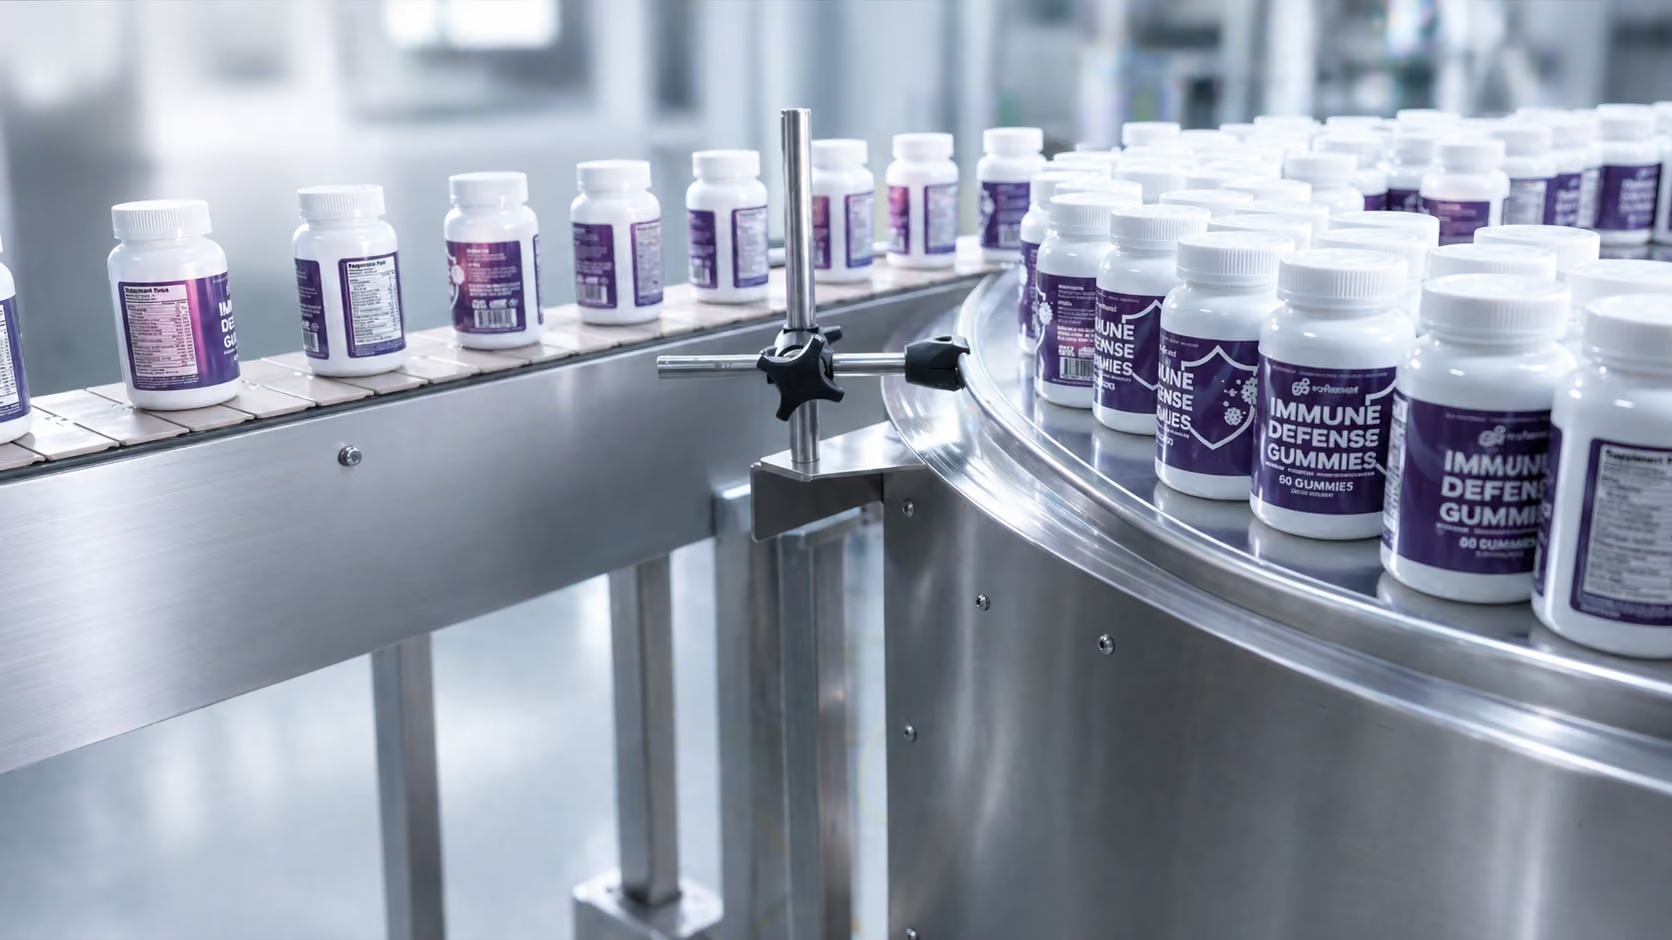
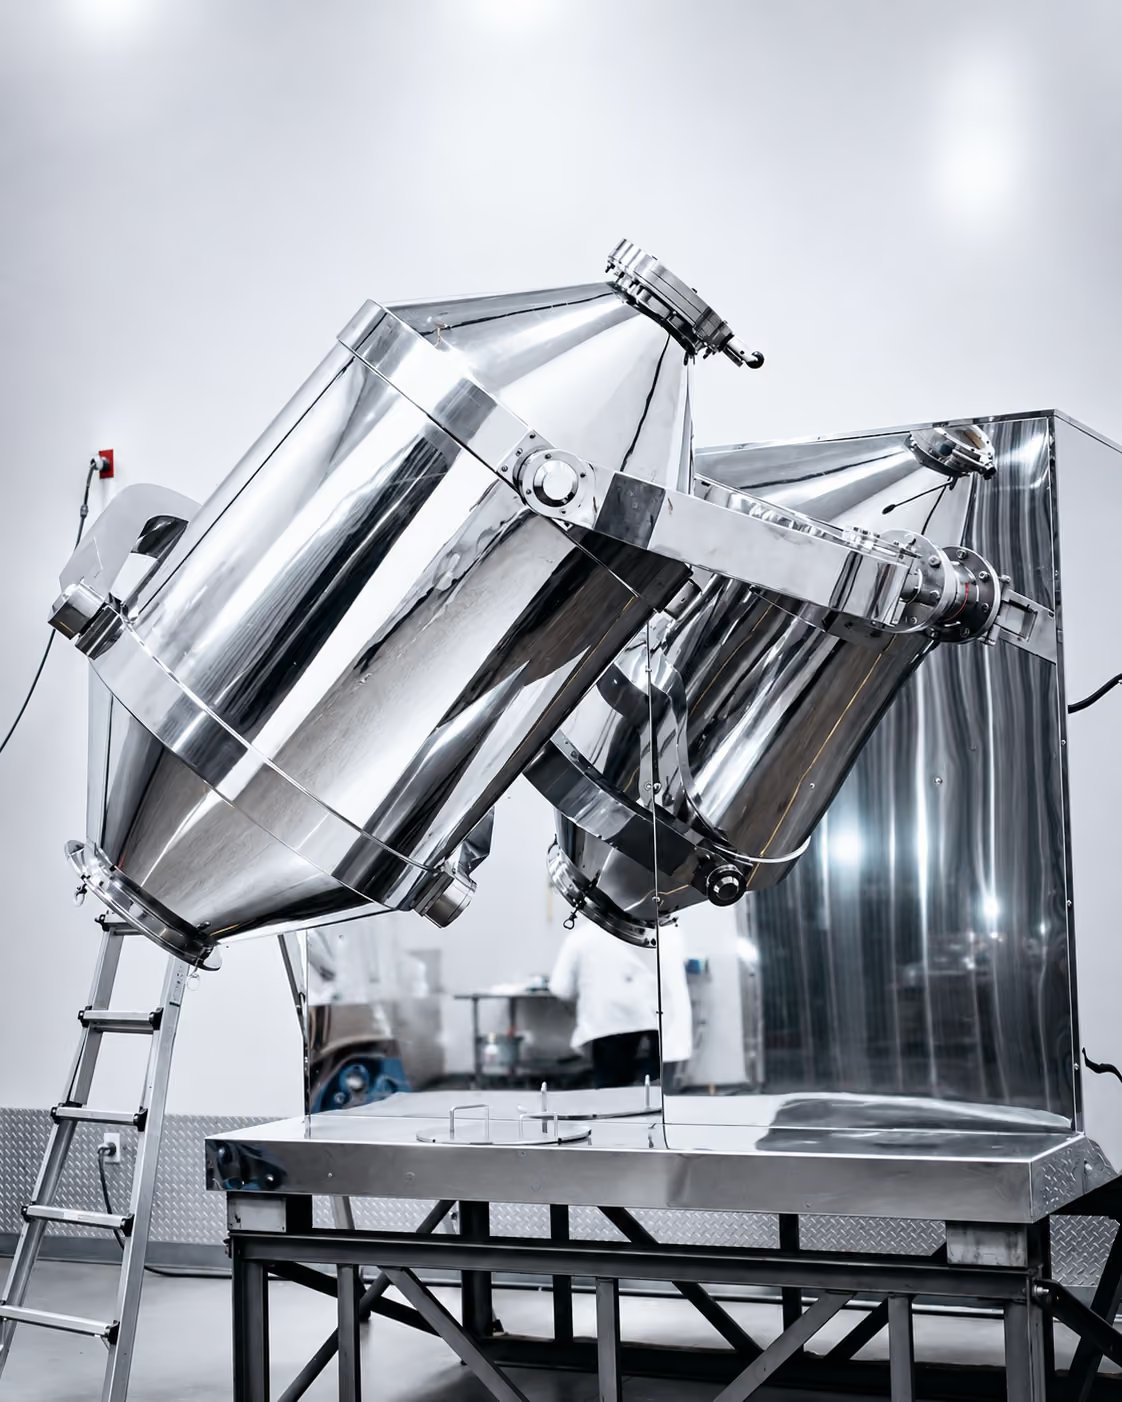
    Inside PAG Pharmatech’s FDA-registered Springville, Utah plant: precision powder blending, high-speed container packaging, and automated stick-pack lines.

    Protein and pre-workout powder contract manufacturing with stick pack filling Bulk Jar & Stick Pack Filling
    PAG Pharmatech America supplement production line in Utah cGMP Cleanrooms
    Automated supplement manufacturing equipment on the production floor High-Speed Blending
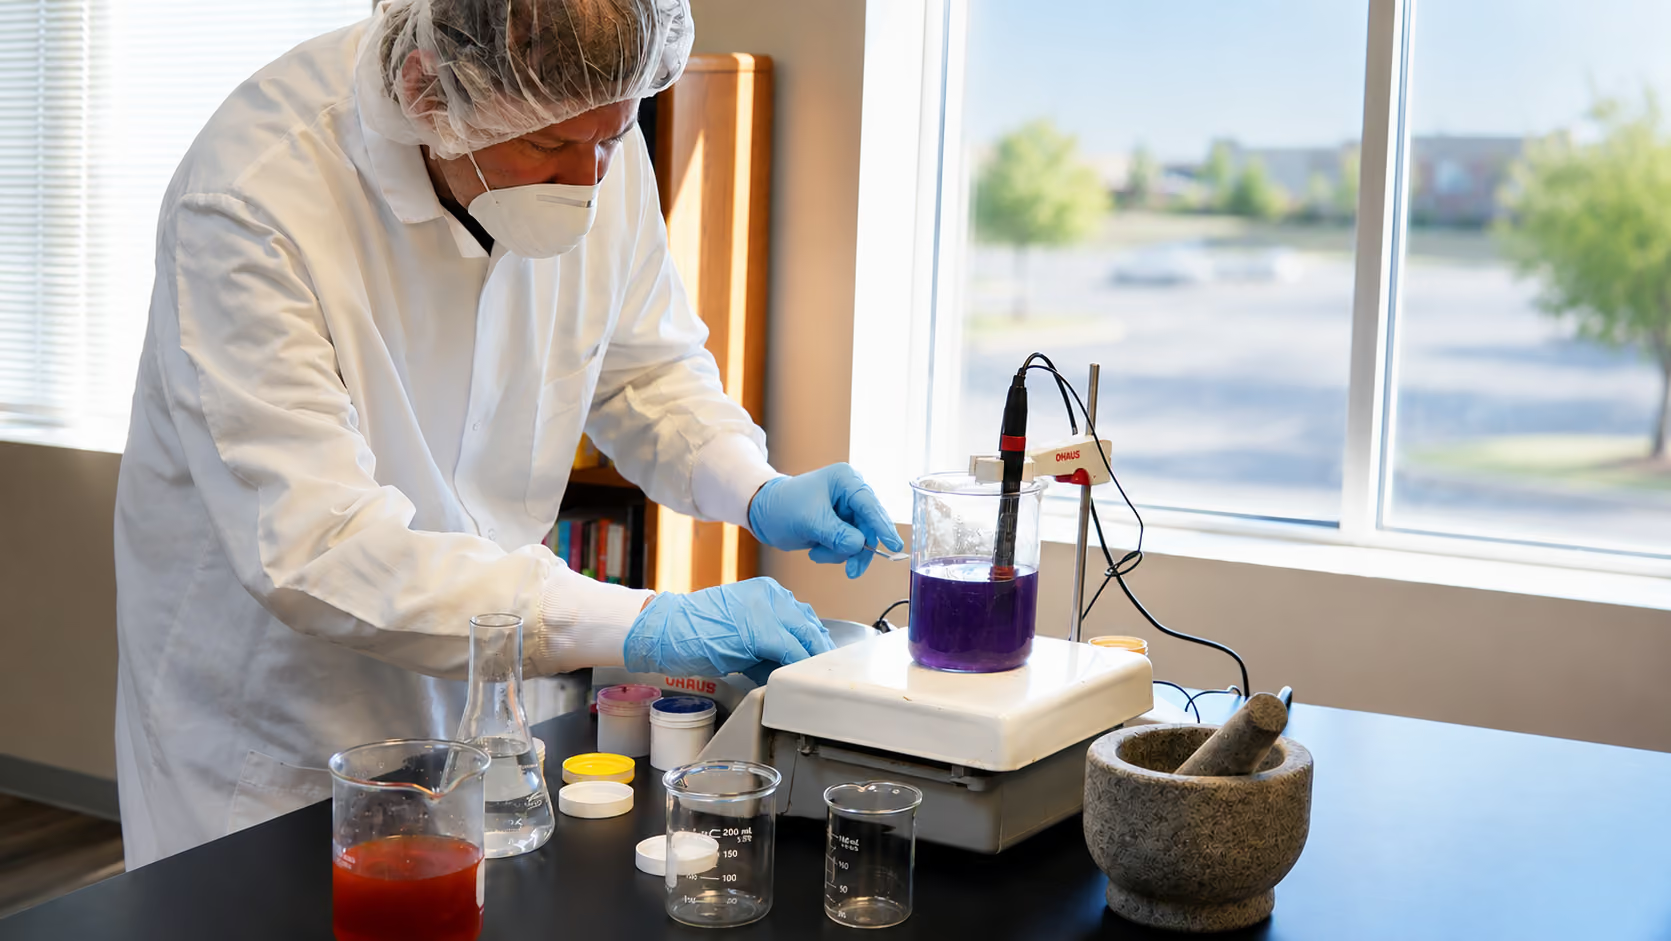
    On-site quality control laboratory for supplement potency testing Analytical Analytical Lab
    Climate-monitored finished goods warehouse for dietary supplements Controlled Storage
    300 kg

    Flexible minimum order quantities tailored for emerging DTC brands, Amazon FBA sellers, and market validation testing.

    Get Catalog
    Strategic Horizon

    Future Procurement Trends in Protein Powder Manufacturing

    Anticipating consumer preference shifts, technological breakthroughs, and supply chain dynamics over the next 5 years.

    1. Clear Protein Technology

    Acid-stable isolates (pH 3.0 to 3.8) are replacing traditional milky shakes. Clear whey and clear plant isolates yield fruit-juice style beverages with ultra-rapid digestion rates and zero milkiness.

    High Growth Shift

    2. Precision Fermentation

    Non-animal dairy proteins created via micro-organism fermentation (identical to whey beta-lactoglobulin) are entering procurement channels, offering animal-free dairy performance with zero lactose.

    Sustainability Focus

    3. Ultra-Clean Labeling & Stevia Rebaudioside M

    Consumers are demanding zero artificial sweeteners (Sucralose, Acesulfame-K) and zero gums (Xanthan, Guar). Modern formulation relies on Reb-M, Monk Fruit, and enzymatic flavor modifiers.

    Clean-Label Standard

    4. Single-Serve & On-the-Go Packaging

    While 2lb and 5lb tubs remain staples, high-speed stick pack sachets and flexible gusseted stand-up pouches are expanding due to lower freight carbon footprints and e-commerce convenience.

    Packaging Innovation
    Company Advantages

    Why Sourcing Directors Partner with PAG Pharmatech America

    We remove structural supply chain risks by combining domestic US manufacturing with global raw material sourcing and absolute regulatory transparency.

    01

    FDA-Registered Utah Infrastructure (21 CFR 111 & 117)

    Operating in Springville, Utah, our cleanroom blending environments maintain positive air pressure, HEPA filtration, and strict climate controls to keep relative humidity ($RH < 40\%$) optimal for powder handling.

    02

    SQF Edition 9 & cGMP Certification

    Audited by third-party bodies including SGS, our quality management system guarantees batch-to-batch repeatability, full lot traceability, and rigorous raw material qualification before production.

    03

    Organoleptic & Flavor Science Lab

    In-house flavor chemists specialize in masking bitter peptides, sulfurous plant notes, and botanical astringency using natural masking agents, spray-dried flavor carriers, and mouthfeel enhancers.

    04

    PAG Global Integrated System (USA · EU · CN)

    Scale seamless from a 300 kg domestic launch in Utah to commercial metric-ton containers in our Netherlands (EU-GMP) or Shenzhen facilities without reformulating or changing specification sheets.

    0 Days
    Accelerated concept-to-market protocol for private label protein powders
    < 0.005 ppm
    Ultra-low ICP-MS heavy metal detection threshold for Prop 65 compliance
    0%
    Full transparency CoA with HPLC, FTIR identity, and micro testing on every batch
    Get Catalog

    Optimized for sales across premier retail & e-commerce platforms

    Amazon
    Walmart Marketplace
    Shopify
    TikTok Shop
    Instagram Shopping
    eBay
    Temu
    Procurement Intelligence

    Private Label Protein Powder Manufacturing FAQs

    Technical, commercial, and regulatory questions answered by our CDMO engineering team.

    Our standard minimum order quantity for powder blending starts at 300 kg per custom formula flavor. For rigid HDPE/PET containers (such as 2lb or 5lb jars), this equates to approximately 300 to 500 units depending on scoop size and serving weight. For single-serve stick packs or sachets, MOQs start at 10,000 units. These low starting thresholds allow emerging DTC brands and Amazon sellers to run market testing without tying up massive capital in inventory.

    Plant proteins (particularly organic pea and brown rice isolates) naturally absorb minerals from the soil. PAG Pharmatech employs strict raw material vendor qualification. Every lot of incoming plant raw material undergoes High-Performance Liquid Chromatography (HPLC) and Inductively Coupled Plasma Mass Spectrometry (ICP-MS) testing. We verify that finished products comply strictly with US FDA regulations and California Proposition 65 thresholds (Lead <0.5 mcg/day, Cadmium <4.1 mcg/day, Arsenic <10 mcg/day).

    For established private label base formulas, lead time is 8 to 10 weeks. For custom formulations requiring custom flavoring, debittering R&D, or specialized active ingredient incorporation (e.g., digestive enzymes, probiotics, adaptogens), lead times run 12 to 16 weeks. This includes lab prototyping, pilot benchtop samples, accelerated stability testing, raw material acquisition, cGMP production, and analytical Quality Assurance release.

    Solubility is governed by particle size engineering and surface tension. We utilize instantized protein raw materials treated with non-GMO sunflower or soy lecithin micro-coatings (fluidized bed spray agglomeration). Additionally, we optimize mesh particle size distribution between 60 and 100 mesh and carefully calibrate anti-caking agents like silicon dioxide when required, ensuring complete dispersion in shaker cups within 10 to 15 seconds without chalky residue.

    We provide comprehensive primary and secondary packaging capabilities:
    • Wide-mouth HDPE / PET Jars (ranging from 16 oz to 5 lb) with induction-sealed pressure liners.
    • Flexible stand-up pouch bags (gusseted zipper pouches) reducing shipping bulk weight.
    • Single-serve stick pack sachets (10g to 45g per packet) ideal for travel and trial kits.
    • Custom printed outer display boxes and shrink-sleeved containers.

    Yes. Over 60% of our production runs are clean-label formulations. We utilize natural high-intensity sweeteners including Stevia Rebaudioside M (Reb-M), organic Stevia Rebaudioside A (Reb-A), and Monk Fruit extract (Mogroside V). We also avoid artificial food dyes, employing natural colorants such as beet root powder, turmeric extract, spirulina, and cocoa powder alkalized for neutral pH blending.

    Every finished shipment is released with an official Certificate of Analysis (CoA) issued by our ISO/IEC 17025 accredited laboratory network. The package includes raw material identity testing (FTIR), finished product active assay potency, microbial screening (Total Plate Count, Yeast & Mold, E. coli, Salmonella, S. aureus), heavy metal analysis, allergen control statements, and full cGMP Batch Production Records (BPR).

    Global CDMO System

    Seamless Protein Manufacturing Across 3 Continents

    Expand your brand footprint effortlessly with PAG's multi-regional CDMO infrastructure in the United States, Netherlands, and China.

    Springville, Utah — USA

    FDA-registered, cGMP, and SQF Edition 9 plant. Primary hub for domestic US brands needing fast domestic shipping, short lead times, and zero tariff overheads.

    Primary US Plant

    The Netherlands — EU Facility

    EU-GMP compliant plant supporting European market entry, EFSA claim compliance, and localized distribution across the European single market.

    European Hub

    Shenzhen — High-Volume Hub

    Strategic scale facility providing raw material sourcing synergy, high-volume capacity, and global export packaging capabilities.

    Global Scale
    Get Catalog

    Ready to Launch Your Private Label Protein Powder Line?

    Connect directly with our technical formulation team in Springville, Utah. Receive custom formulation feedback, cost estimates, and product spec sheets within 24 business hours.

    FDA registration does not constitute FDA approval or endorsement of any product. Certifications are held by our FDA-registered manufacturing operation; certificate copies are available under NDA during supplier qualification.