An authoritative technical analysis on compliance frameworks, cross-border regulatory harmonisation, advanced biopharmaceutical delivery systems, and risk-mitigated procurement for enterprise brand owners.
In the contemporary B2B health and wellness landscape, securing a contract development and manufacturing organization (CDMO) that bridges technical expertise with certified regulatory integrity is paramount. While CE marking traditionally governs machinery compliance, cleanroom air processing units, and high-precision packaging automation within European directives, its operational integration into modern nutraceutical facilities serves as a core benchmark for engineering excellence.
Enterprise procurement directors must navigate a complex multi-jurisdictional compliance matrix. Operating under strict adherence to US FDA 21 CFR Part 111 (Dietary Supplements cGMP) and 21 CFR Part 117 (Preventive Controls for Human Food), alongside SQF Edition 9, HACCP, and ISO 22000 specifications, our integrated manufacturing framework eliminates trade friction across North American, European, and Asia-Pacific supply chains.
“Information Gain Advantage: Regulatory compliance is no longer a post-production checklist—it is an embedded molecular-to-pallet QA protocol that mitigates customs seizures, retailer rejections, and inventory write-offs.”
By enforcing strict raw material qualification, FTIR identity verification, inductively coupled plasma mass spectrometry (ICP-MS) heavy metal screening, and real-time microbial testing, brand owners achieve full batch-level traceability and regulatory confidence.
| Compliance Standard | Governing Body | Strategic Benefit for Buyers |
|---|---|---|
| CE Certification | European Standards (EU) | Guarantees cleanroom equipment safety, automated precision & EU market hardware alignment. |
| FDA 21 CFR 111 / 117 | US FDA | Full cGMP compliance, sanitary hazard analysis & mandatory identity/potency verification. |
| SQF Edition 9 | GFSI Recognized | Comprehensive food safety management required by major global retail chains and supermarket networks. |
| HACCP & ISO 22000 | International Standards | Systematic hazard prevention, standardized operational processes, and global trade audit readiness. |
| Halal & Kosher | Global Religious Councils | Expanded market access into specialized demographic and international consumer segments. |
Explore our top-tier private label formulations and turnkey manufacturing solutions engineered for rapid deployment across DTC, Amazon, and international retail channels.
Premium grade polyoxyethylene ether thickener engineered for high-viscosity personal care, topical formulations, and specialized cosmetic emulsions.
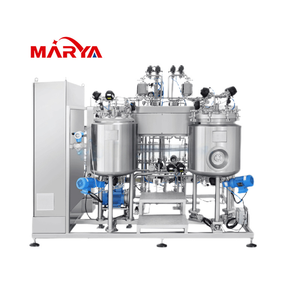
Turnkey biopharmaceutical and nutraceutical processing system supporting complex liquid, suspension, and powder dosage formulations.
Standardized 10:1 ratio Taraxacum officinale extract powder for liver health, detoxification blend formulations, and herbal capsules.
Pea, brown rice, and pumpkin seed protein blends with zero artificial sweeteners, complete amino acid profile, and fast instantization.
High-efficiency fluorescent brightening agents developed under cleanroom parameters for industrial, polymer, and coating applications.
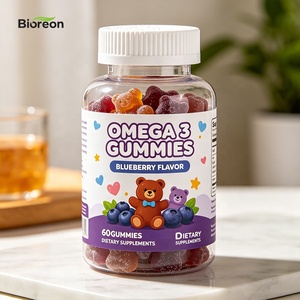
Plant-derived ALA/DHA gummies with citrus natural flavoring, zero sugar alcohols, heat-stable pectin structure, and validated fatty acid stability.
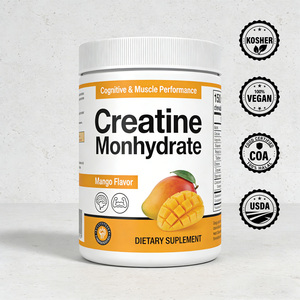
Micronized 200-mesh creatine monohydrate chewable tablets optimized for rapid bioavailability, enhanced athletic performance, and clean label appeal.
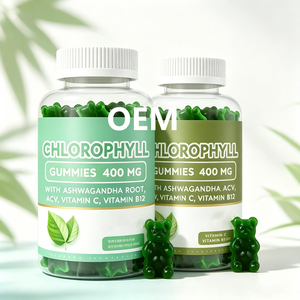
Sodium copper chlorophyllin rich green gummies for internal deodorization, cellular wellness, and antioxidant defense. Available in custom flavors.
From micro-encapsulated active powders to nitrogen-flushed liquid softgels, our Springville plant operates automated production suites engineered for maximum potency retention and thermal protection.
Continuous starchless deposit technology capable of handling heat-sensitive vitamins, probiotics, and botanical extracts. Includes sugar-free maltitol and clean-label citrus pectin platforms.
MOQ: 6,000 UnitsHigh-speed planetary ribbon blending and automated sachet packaging for pre-workout formulas, collagen peptides, green superfoods, and hydration electrolyte systems.
MOQ: 300 kgHigh-tonnage rotary tablet presses delivering compressed, chewable, enteric-coated, and effervescent tablets with strict friability and dissolution profile parameters.
MOQ: 5,000 UnitsRotary die encapsulation for lipid-soluble compounds, Omega-3 fish oils, CoQ10, MCT oil, and Astaxanthin with nitrogen blanketing to prevent lipid peroxidation.
MOQ: 5,000 UnitsAutomatic encapsulation lines processing sizes 000, 00, 0, and 1 in both non-GMO HPMC vegetable shells and bovine gelatin with optional band-sealing technology.
MOQ: 5,000 UnitsCold-extruded functional soft chews for canine and feline joint health, calming, and coat nutrition formulated in compliance with NASC and AAFCO guidelines.
MOQ: 2,000 UnitsData-driven forecast on ingredient innovation, bio-delivery systems, clean label mandates, and risk management strategies for executive decision-makers.
The consumer market has shifted from basic ingredient inclusion to verified blood-plasma absorption rates. Conventional oral delivery of unstable compounds—such as Glutathione, Curcumin, and Vitamin C—suffers severe degradation in the gastrointestinal tract. Enterprise buyers are increasingly turning to liposomal phospholipid encapsulation and spray-dried microencapsulation. Our CE-certified high-pressure homogenization lines ensure sub-micron particle sizing for maximum cellular uptake and extended shelf-life stability.
While gelatin gummies dominated early market share, regional climate volatility and vegan consumer preferences have driven massive demand for citrus-pectin and tapioca-based matrices. Next-generation gummy formulations replace traditional corn syrup with soluble corn fiber, erythritol, and monk fruit. Furthermore, specialized thermal curing techniques prevent gummy melting during cross-border tropical transit, safeguarding brand integrity across direct-to-consumer delivery networks.
Heightened regulatory scrutiny in California (Prop 65) and European FSA directives has elevated heavy metal oversight to an all-time peak. Sourcing raw materials without verified ICP-MS certification exposes brand owners to massive legal liabilities. Modern contract manufacturing requires full transparency: every production batch must be accompanied by an exhaustive Certificate of Analysis (CoA) validating non-detectable levels of Lead, Cadmium, Arsenic, and Mercury, alongside zero pesticide residues.
The traditional 6-to-9 month manufacturing cycle is obsolete in modern e-commerce and retail environments. Leading brands leverage integrated CDMO systems where raw material staging, formula optimization, stability testing, primary packaging, and QA batch release are executed within an expedited 90-day window. This speed-to-market advantage allows brand managers to capitalize on viral wellness trends before market saturation occurs.
From our headquarters in Springville, Utah to our global facility network across Europe and Asia, we combine pharmaceutical-grade precision with flexible contract scalability.
Our state-of-the-art facility operates under 21 CFR Part 111 cGMP and Part 117 preventive controls. Cleanrooms maintain positive atmospheric pressure, HEPA air filtration, and continuous relative humidity logging to ensure zero cross-contamination.
We compress traditional multi-vendor handoffs into a unified master timeline. A dedicated technical project coordinator manages your formulation, packaging die-lines, stability testing, and final QA release under one roof.
Eliminate single-region supply chain vulnerabilities. With production hubs in Springville (USA), an EU-GMP facility in the Netherlands, and a high-volume sourcing hub in Shenzhen, your brand gains localized lead times and zero tariff penalty.
Every raw material lot undergoes raw identity testing via FTIR spectroscopy, HPLC potency verification, and real-time microbial plating before entering our blending suites. Certificates of Analysis are generated directly from validated empirical data.
Complete primary and secondary packaging capabilities: HDPE/PET bottles, glass jars, induction-sealed pouches, blister packs, and multi-count stick pack cartons featuring custom lot coding, tamper-evident shrink sleeve application, and Amazon FBA compliance.
We empower scaling DTC brands and enterprise brand line extensions alike. Sized accessibility starting at 6,000 units for gummies and 5,000 units for capsules/tablets allows rapid market validation prior to committing to high-volume production runs.
Get instant clarity on technical specifications, regulatory documentation, minimum order quantities, and international order processing.
Consult directly with our Utah-based formulation scientists and regulatory team today. Receive a transparent price quotation, technical bill of materials (BOM) review, and sample plan within 24 business hours.
Contact Us