US-Based Supplement Manufacturing  ·  FDA-Registered & GMP Certified  ·  8–12 Week Lead Times
FDA Registered SQF Ed. 9 Halal & Kosher 30 Years CDMO
Springville, Utah · Technical R&D Center

Custom Supplement Formulation R&D: Scientific CDMO Excellence

How global health brands engineer bioavailable, stable, and compliant nutraceuticals. From molecular synergism and organoleptic balancing to 90-day commercial cGMP production in Utah.

21 CFR 111 & 117 cGMP SQF Ed. 9 & In-House Analytical Lab Zero Third-Party Broker Hand-Offs

Custom Formulation R&D Benchmarks

0
Days from concept brief to commercial launch
0+
Custom formulations engineered in North America
0
Commercial delivery form platforms
0+
Years of global pharmaceutical & CDMO heritage

In-house formulation chemists specializing in novel bioavailability

Real-time & accelerated stability predictive modeling (40°C / 75% RH)

Complete Supplement Facts panel & FDA claim audit

0 Days
R&D Brief to Scale-Up
0%
In-House Analytical Testing
0%
On-Time Batch Release
0 Global
Integrated Operations (USA/EU/Asia)
FDA-Registered Utah Plant GMP & SQF Edition 9 Certified Accelerated Stability Screening Global CDMO Network Clean Label & Vegan Specialists
Scientific Formulation Architecture

The Anatomy of Custom Supplement Formulation R&D

Generic contract manufacturers rely on stock pre-blends that compromise active potency and bio-accessibility. PAG Pharmatech approaches R&D through rigorous pharmaceutical chemistry, ingredient thermodynamics, and kinetic stability engineering.

1. Molecular Synergism & Overages

Formulating active botanicals, minerals, and vitamins requires calculating kinetic degradation pathways. We perform precise overage modeling so your label claim is 100% compliant at month 24 without causing gastrointestinal distress or physical instability.

2. Delivery Matrix Engineering

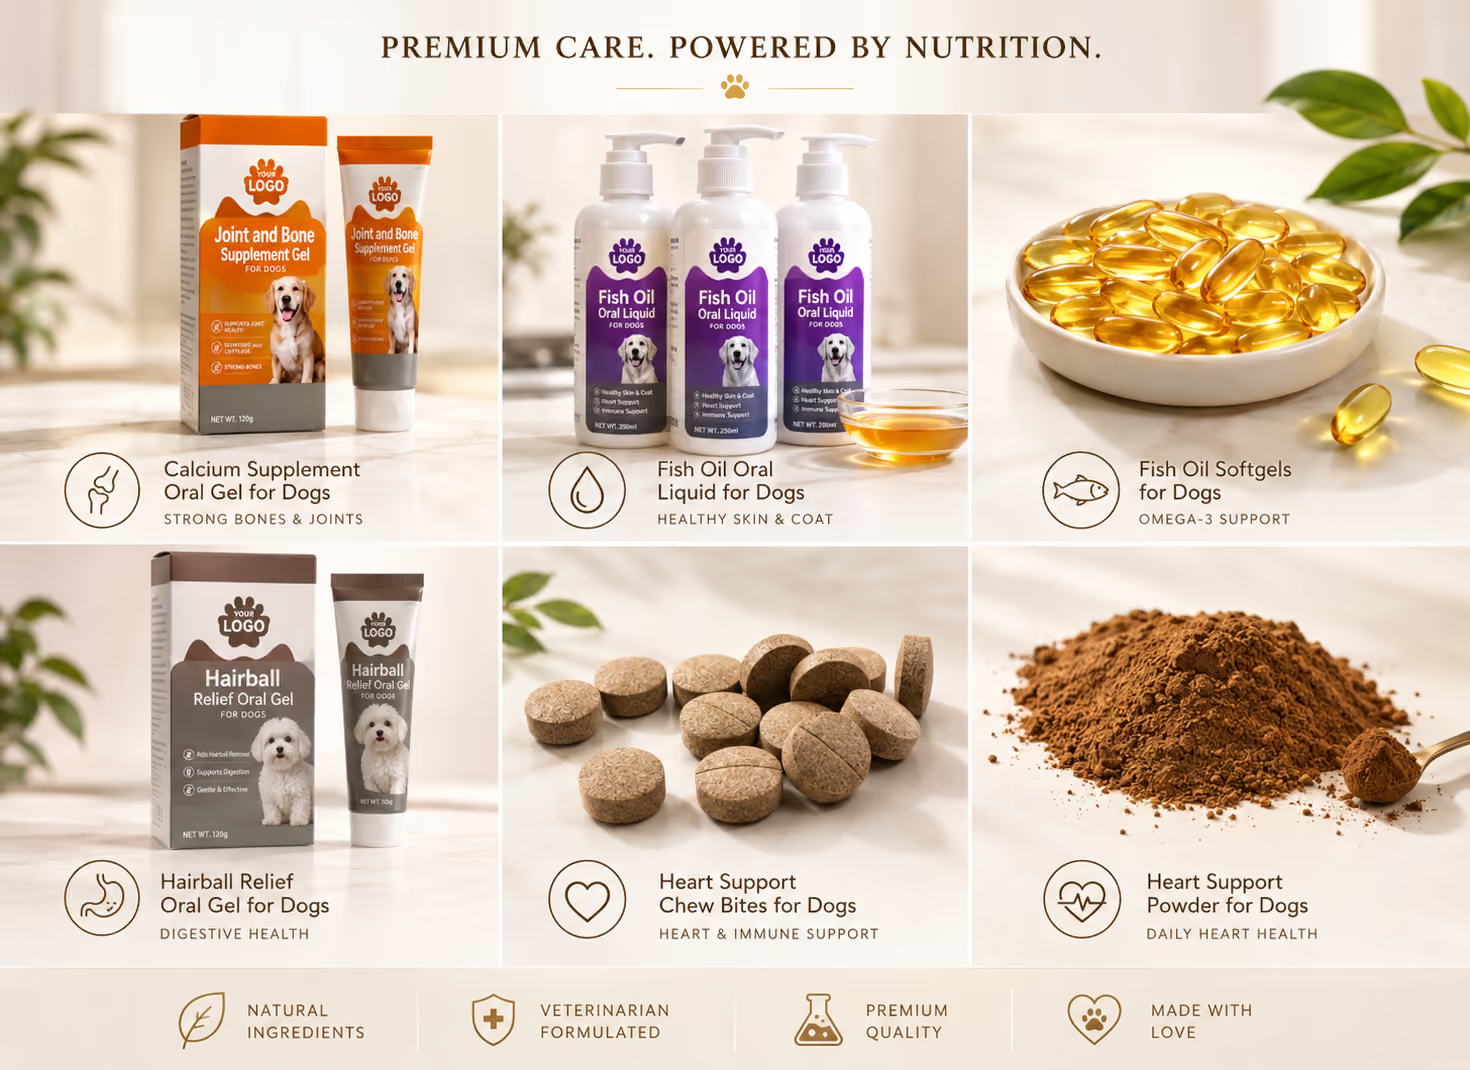
Selecting between HPMC veggie capsules, non-GMO pectin gummies, lipophilic softgel suspensions, or instantized soluble powders depends on the logP value and hydrophobic properties of your active compounds.

3. Taste & Organoleptic Masking

High-dose botanical extracts, amino acids, and minerals exhibit intense bitterness, astringency, or metallic off-notes. Our flavor chemists employ natural microencapsulation, pH modification, and targeted aroma technology to build smooth profiles.

4. Stress Stability & Shelf-Life

Prior to pilot production, custom prototypes undergo accelerated thermal testing (40°C at 75% relative humidity) alongside water activity (aW) analysis to prevent clumping, cross-linking, active precipitation, or microbial proliferation.

Formulation Insight: Hydrophobic Actives & Bioavailability

When developing custom formulations containing lipophilic actives like Curcumin, CoQ10, Resveratrol, or Vitamin D3, traditional powder blending yields less than 10% intestinal absorption. Our R&D laboratory specializes in self-emulsifying drug delivery systems (SEDDS) and lipid-bound micellar dispersions. By incorporating specific phospholipids and natural surfactant matrices, we increase active bio-accessibility by up to 500% while retaining clean-label compliance for retail markets.
Omnichannel distribution platforms for our custom formulations

Amazon Compliance Formulation R&D
Walmart Retail Formulation R&D
Shopify DTC Custom Formulation
TikTok Shop Viral Supplement Formulation
Instagram Health Brand R&D
Global Marketplace R&D
Cross-Border E-Commerce R&D
Market Intelligence & Procurement Insights

Future Trends in Custom Supplement Formulation & Sourcing

Procurement managers and brand directors must navigate evolving consumer expectations, shifting regulatory hurdles, and ingredient supply bottlenecks. Here is how custom R&D is transforming for 2026 and beyond.

1. Precision Bio-Fermentation Actives

Procurement is shifting away from raw crude extracts toward high-purity bio-fermented active compounds like Ergothioneine, Urolithin A, and NAD+ precursors (NMN/NR). Formulation R&D requires precise thermal and moisture controls to preserve molecular integrity during mass production.

Next-Gen Bioactives

2. Clean-Label Polymer Innovations

Consumers reject synthetic binders, silicon dioxide, and magnesium stearate. Advanced R&D now utilizes organic tapioca maltodextrin, rice hull concentrates (Nu-RICE®), and sunflower lecithin to achieve optimal powder flowability and tablet hardness without artificial additives.

Clean-Label Excipients

3. Supply Chain Decoupling & Multi-Sourcing

Relying on a single geographic region for raw material sourcing introduces massive lead-time volatility. Leading brands partner with CDMOs capable of dual-sourcing pre-audited raw materials across the US, Europe, and Asia, ensuring seamless batch continuity.

Supply Resilience

E-E-A-T Quality Principle: Amazon & Retail Audit Readiness

Formulations without verified analytical testing risk instant removal from platforms like Amazon, Walmart, and Target. Our R&D framework embeds ISO/IEC 17025 accredited analytical validation into every custom formulation project—providing heavy metal screen (ICP-MS), potent active assay (HPLC), pesticide residue screen, and microbial challenge testing upfront.

Contact Us
R&D Stage-Gate Execution

The 90-Day Custom Formulation Path

From initial feasibility assessment to final cGMP commercial batch release, our Utah-based technical team eliminates lead-time friction through structured Stage-Gate project management.

01

Formulation Feasibility & Theoretical BOM (Days 1–14)

Our chemists analyze target label claims, dosing parameters, solubility requirements, and cost-per-serving targets to construct a validated Bill of Materials (BOM).

02

Lab Prototype & Flavor Optimization (Days 15–30)

We produce benchtop prototypes for organoleptic review, disintegrating testing, physical integrity validation, and initial active potency verification.

03

Accelerated Stability & Pilot Scaling (Days 31–60)

Prototypes are subjected to thermal stress testing (40°C / 75% RH) alongside pilot runs on full-scale production machinery to optimize flow, encapsulation, or depositing.

04

cGMP Commercial Production & QA Release (Days 61–90)

Full batch production inside our FDA-registered plant, accompanied by a complete Certificate of Analysis (CoA) and master batch production records.

0 Days
Guaranteed execution timeline from NDA execution to finished pallets
0%
Traceability on all raw materials with pre-screened Certificate of Analysis
0
Third-party brokers involved—direct line to Utah R&D bench chemists
Contact Us
Enterprise Manufacturing Infrastructure

Springville, Utah R&D & Commercial Facility

Our state-of-the-art facility features climate-monitored cleanrooms, automated dosage machinery, and an in-house quality testing laboratory built for rapid iteration and high-volume commercial scale-up.

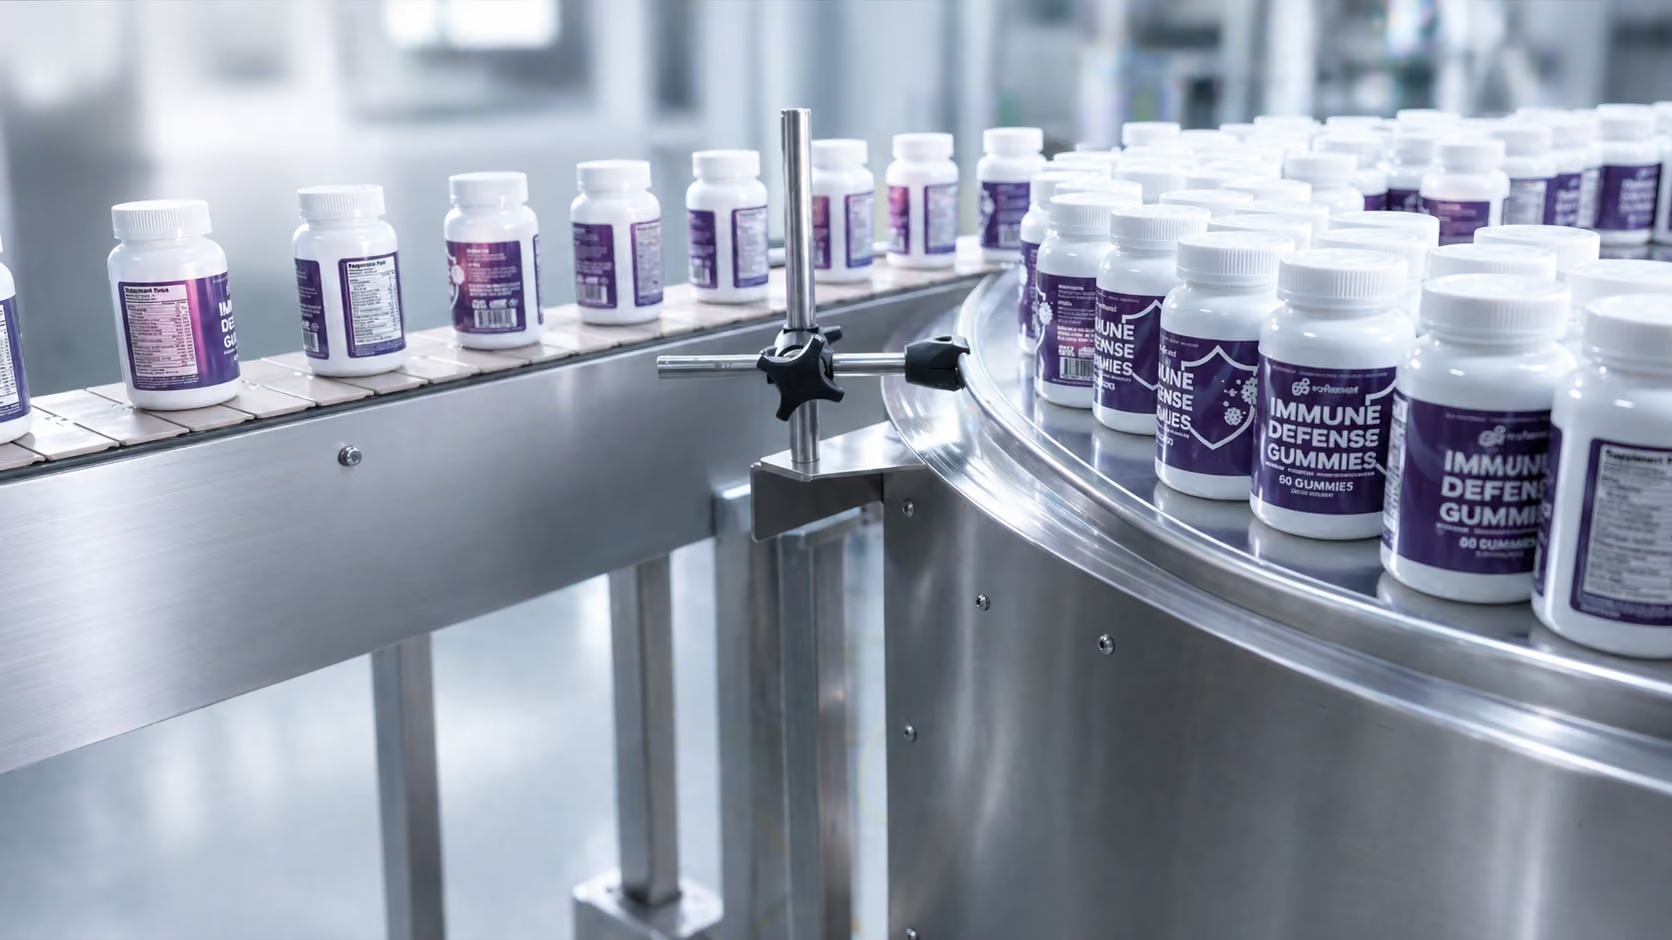
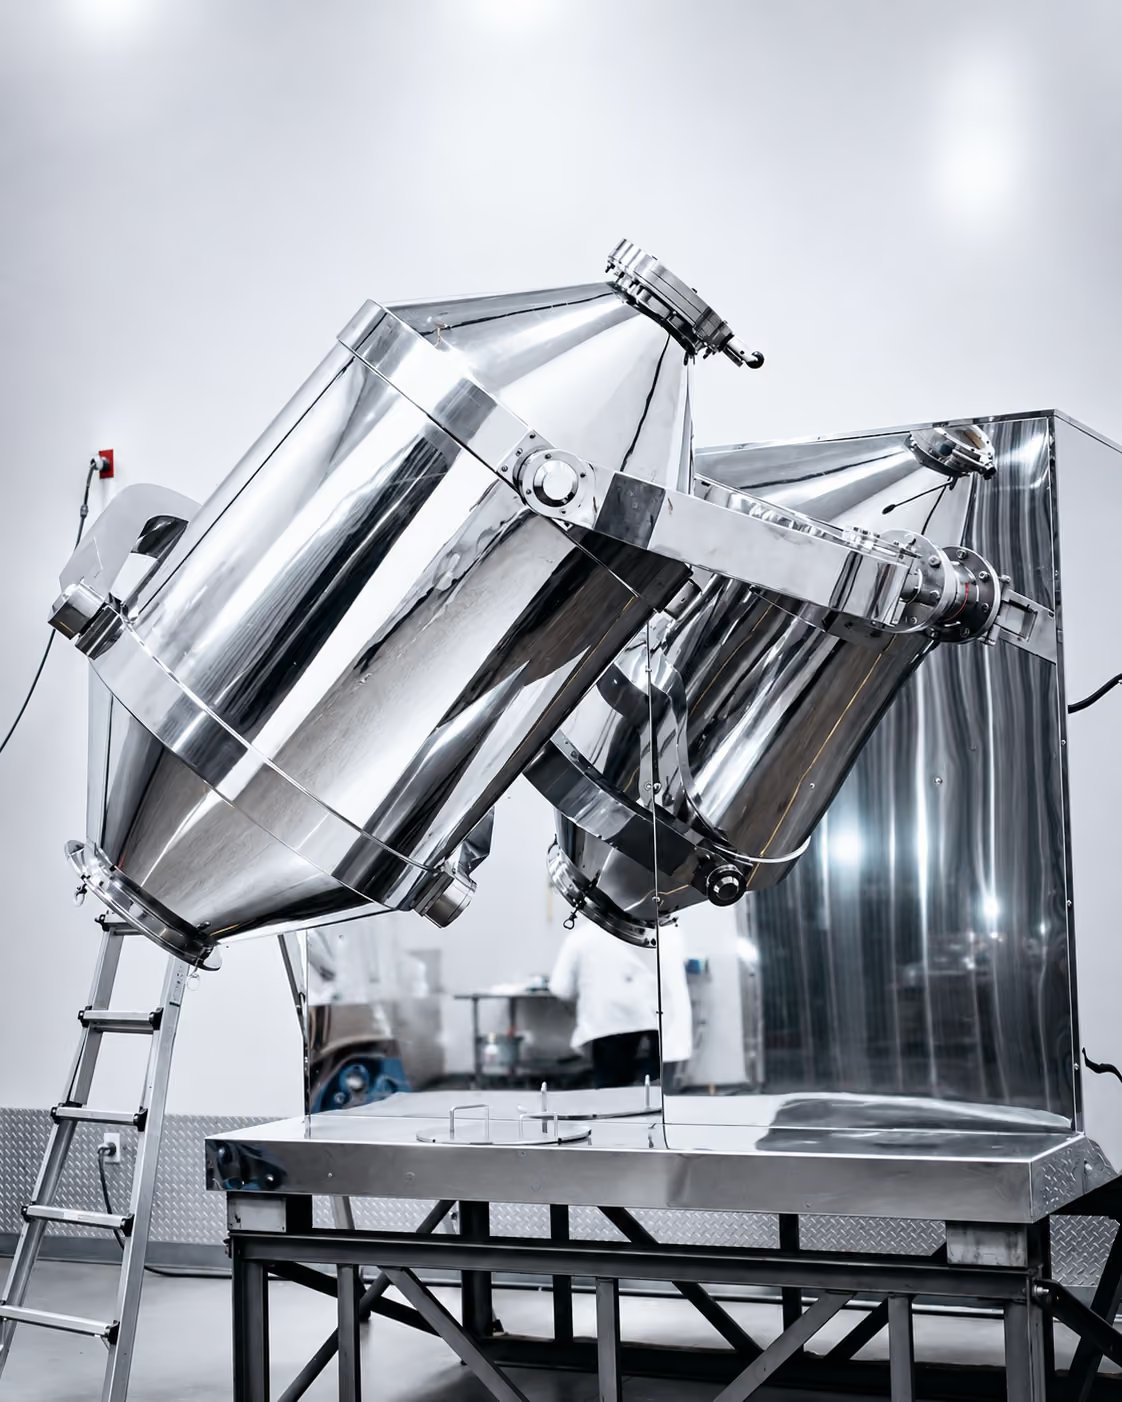
Utah cGMP production suite for custom supplement formulation R&DcGMP Production Suites
High-speed supplement encapsulation and tableting equipmentAutomated Scaling Machinery
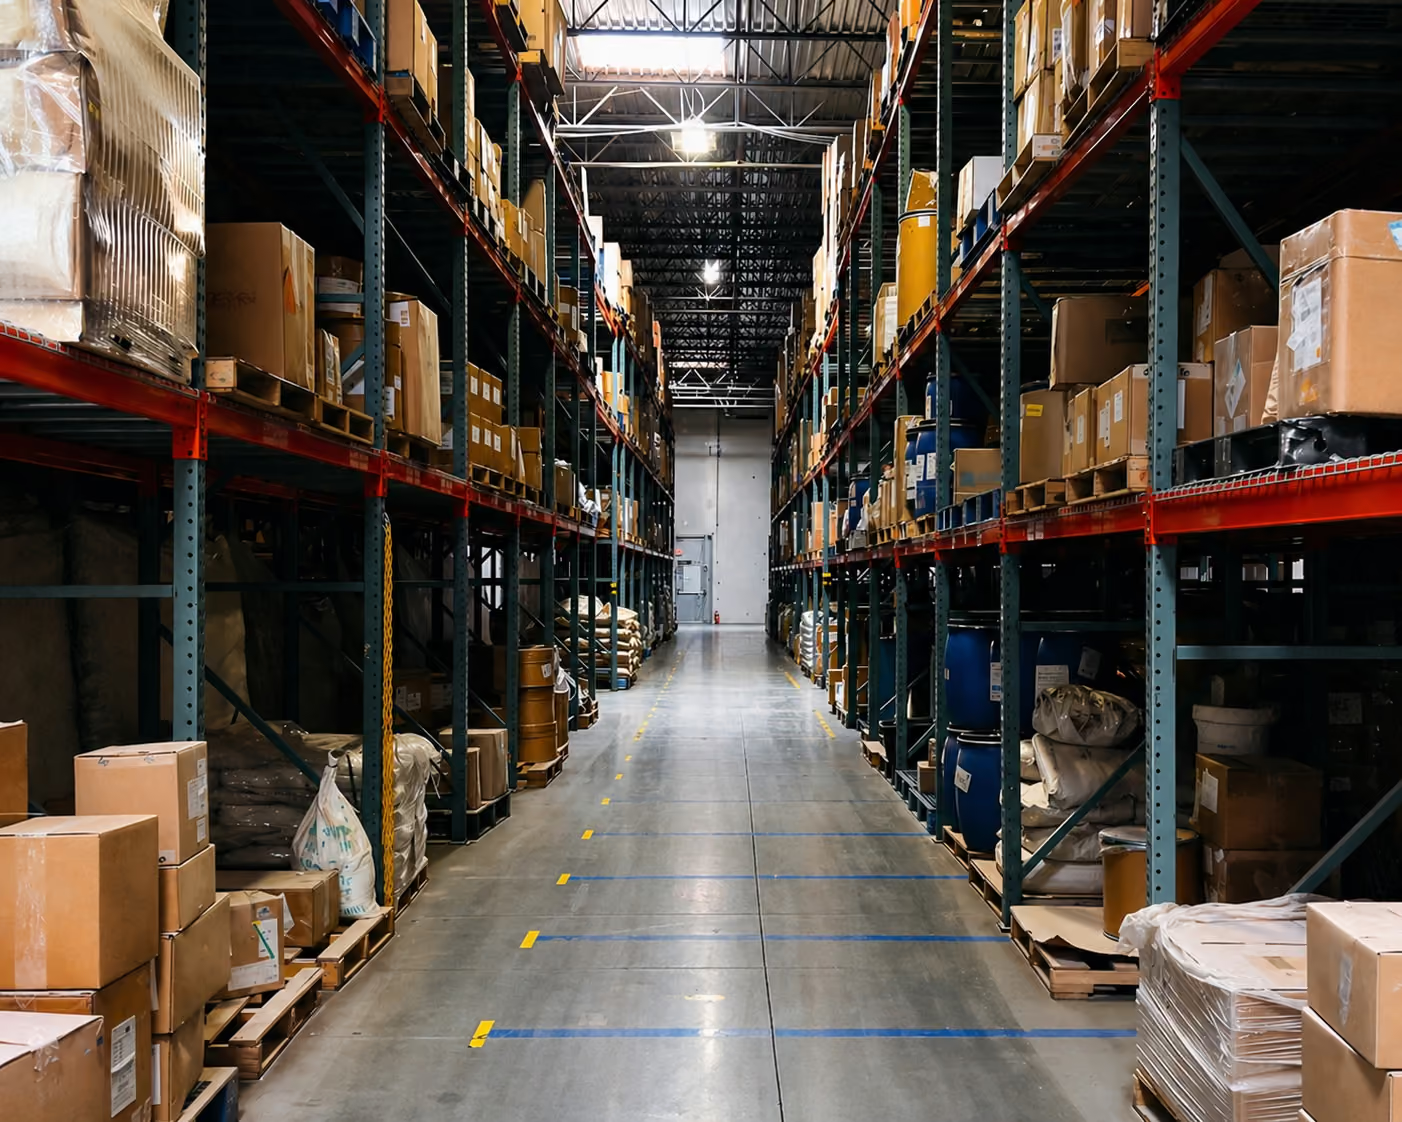
Climate-controlled finished goods warehouse for dietary supplementsClimate-Controlled Storage
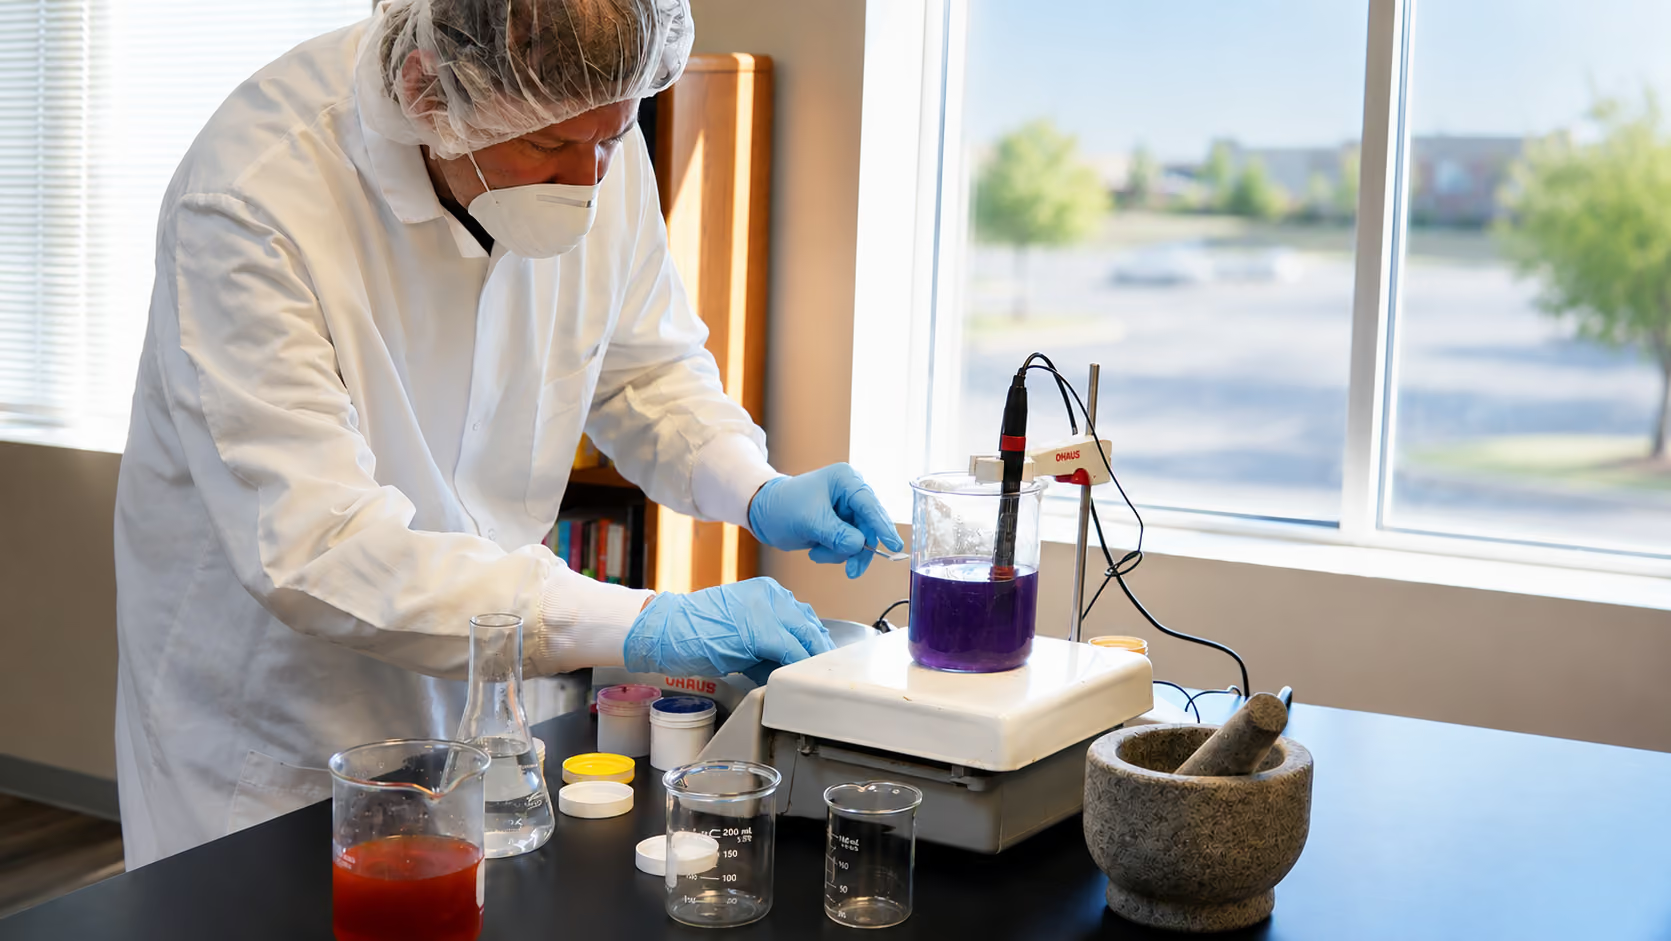
In-house analytical testing laboratory for supplement potency and heavy metalsAnalytical QC Lab
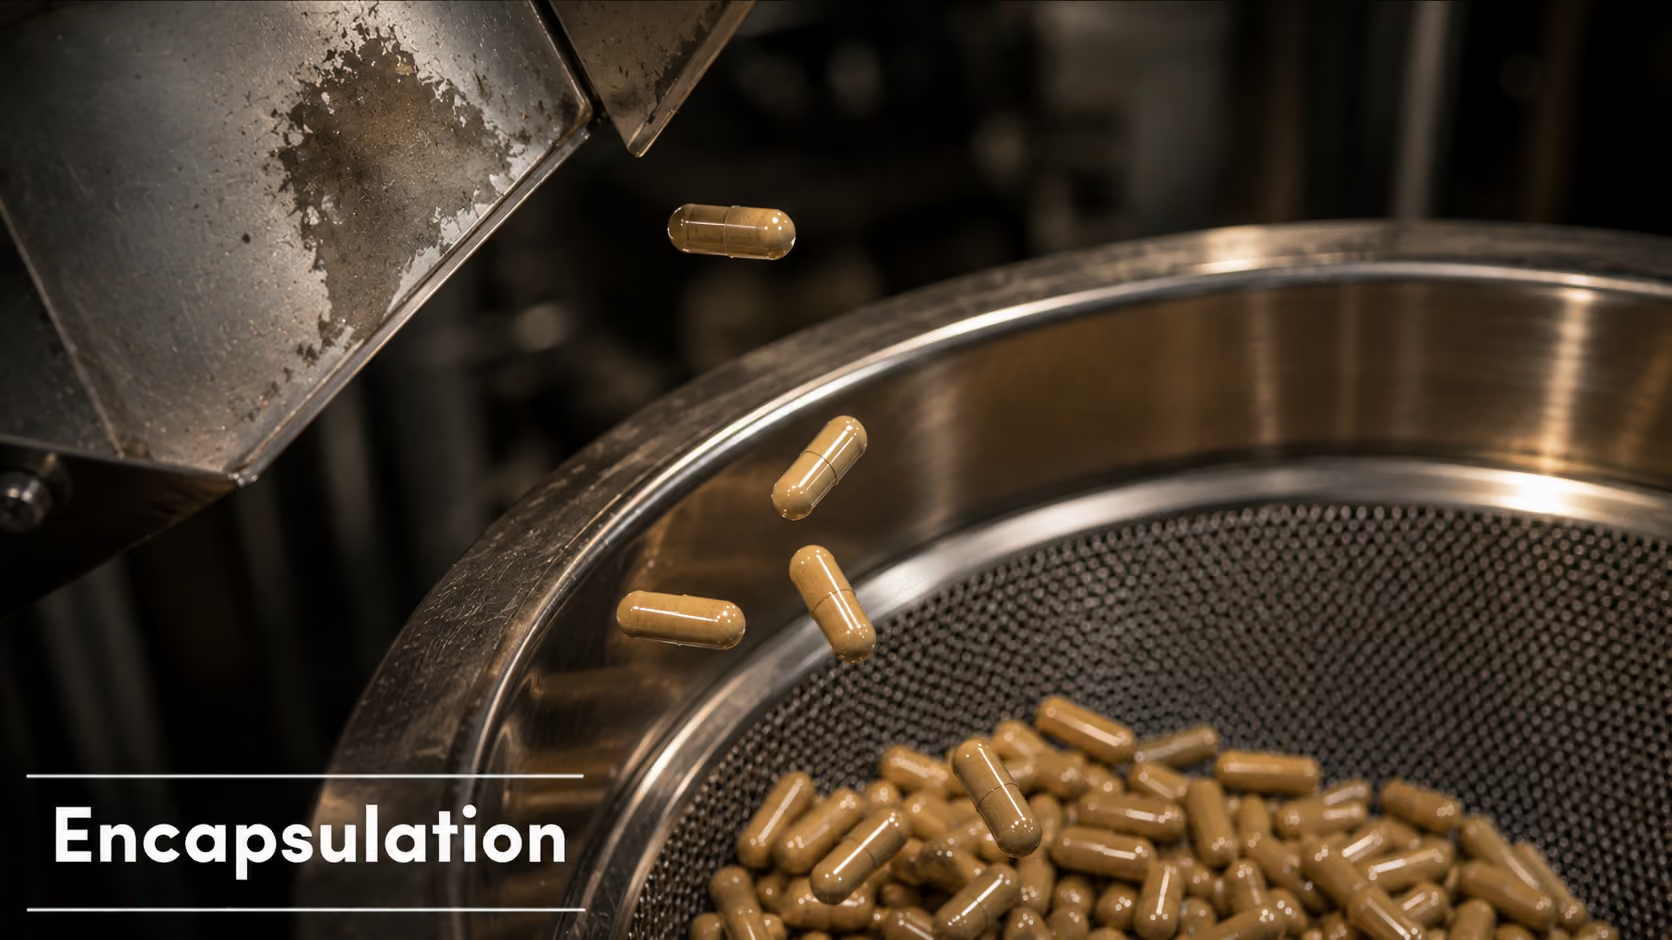
Encapsulation line for HPMC and gelatin hard capsulesPrecision Encapsulation
6

Dosage form platforms fully integrated under one roof in Springville, Utah.

Contact Us
Global CDMO Ecosystem

Integrated R&D Scale across Three Continents

PAG's Global System bridges our US manufacturing hub with specialized European compliance and high-volume Asian raw material sourcing—providing unmatched cost efficiency and supply chain redundancy.

Springville, Utah — Main CDMO HQ

FDA-registered, 21 CFR Part 111 & 117 cGMP, SQF Edition 9 facility. Direct R&D bench support, pilot batch scaling, and domestic 8-12 week order fulfillment.

Primary Commercial Hub

Netherlands — EU-GMP Facility

EFSA & Novel Food compliant formulation adaptation. Serves brands expanding across European union marketplaces with zero regulatory friction.

European Market Entry

Shenzhen — Raw Material Sourcing

Direct supply-chain integration with primary ingredient producers. Ensures high-purity botanical extracts, active raw material verification, and cost optimization.

Sourcing & High Volume
Contact Us
Technical Sourcing & Procurement FAQ

Custom Supplement Formulation R&D Answers

Direct answers to the most critical technical, regulatory, and manufacturing questions asked by brand founders and corporate buyers.

Our R&D team uses precision overage modeling combined with late-stage low-temperature vacuum dosing and microencapsulation. By shielding heat-sensitive botanical extracts and vitamins from peak thermal exposure during pectin gelling (90°C–105°C), we guarantee active potency through full shelf life without sacrificing gel texture.

Technology transfer follows a 4-step cGMP gate system: Bill of Materials (BOM) & raw material equivalency audit, analytical method alignment (HPLC/ICP-MS), pilot scale trial run to verify flowability and compressibility, and formal process validation with 3-batch stability benchmarking.

Our regulatory scientists conduct ingredient safety audits against FDA NDI notifications, GRAS (Generally Recognized As Safe) dossiers, and 21 CFR Part 111 compliance. We verify structural identity, heavy metals, and botanical adulterants before incorporating any novel bioactive into your formula.

We utilize nitrogen-blanketed mixing tanks, lipophilic natural antioxidant systems (mixed tocopherols, rosemary extract, ascorbyl palmitate), and peroxide/anisidine value tracking. Softgel gelatin or HPMC shells are engineered with specific oxygen transmission rates to protect sensitive Omega-3 and CoQ10 actives.

Every custom production batch is released with a comprehensive CoA (Certificate of Analysis) from ISO 17025 accredited testing covering potency, heavy metals, microbiology, residual solvents, pesticides, master batch manufacturing records (MMR), and Amazon-compliant Supplement Facts panel documentation.

Custom R&D prototyping begins with accessible MOQs: 6,000 units for gummies, 5,000 units for tablets, softgels, and hard capsules, or 300 kg for powders and pet nutrition. R&D Bench Fees are fully credited back to your account upon commitment to your first commercial production run.

Build Your Custom Formulation in the USA

Partner with an FDA-registered, cGMP-certified CDMO in Springville, Utah. Receive a comprehensive formula feasibility review, BOM cost estimate, and sampling timeline within 24 hours.

FDA registration does not constitute FDA approval or endorsement of any product. Certifications are held by our FDA-registered manufacturing operation; certificate copies are available under NDA during supplier qualification.