Engineered for Boston life science innovators, direct-to-consumer brands, and clinical supplement buyers requiring verified active recovery, precise potency, and audit-ready documentation.
In the rapidly expanding life sciences corridor of Greater Boston—stretching from Kendall Square in Cambridge to Route 128 and the suburban technology parks of Woburn, Framingham, and Waltham—the demand for precision dietary supplement processing has evolved. Brand owners, clinical researchers, and direct-to-consumer (DTC) wellness companies increasingly rely on Toll Supplement Manufacturing to preserve intellectual property, maintain strict cost governance, and ensure rigorous quality assurance.
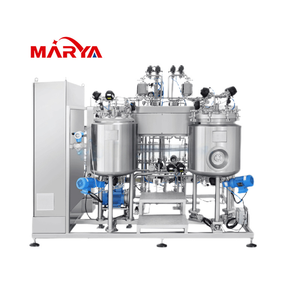
Unlike traditional full-service Contract Manufacturing (where the manufacturer sources all raw materials and owns the foundational formulation parameters), toll manufacturing empowers Boston brands to supply their own proprietary active pharmaceutical ingredients (APIs), specialized botanical extracts, micro-encapsulated nutrients, or patented compounds. As your dedicated toll manufacturing factory partner, PAG Pharmatech America LLC provides the specialized processing infrastructure—including high-shear blenders, automated encapsulation machines, continuous gummy depositing lines, analytical testing laboratories, and cleanroom environments—while adhering strictly to customer-provided Master Batch Records (MBRs) and Technology Transfer Protocols.
You supply the raw active ingredients (e.g., purified dandelion extract, vegan omega-3 oils, custom thickeners like Crothix), retaining complete ownership of raw material vendor sourcing and margin control.
Execution takes place inside our FDA-registered facility under 21 CFR Part 111 (dietary supplements) and Part 117 (preventive controls for human food), backed by SQF Edition 9 protocols.
Streamlined tech transfer methodologies allow Boston formulation teams to move seamlessly from benchtop R&D samples to commercial-scale 500kg pilot runs in under 30 business days.
By utilizing toll manufacturing services tailored for the Massachusetts market, procurement teams eliminate capital expenditures on heavy machinery, reduce overhead, and overcome regional labor bottlenecks, all while maintaining rigorous oversight over their core chemical and biological formulations.
Boston is unique. As an international epicenter for biomedical research, Harvard/MIT academic spin-offs, and health-conscious consumer populations, the regional market demands a higher standard of nutraceutical engineering than standard mass-market supplement channels. Boston brand owners are currently leading national shifts in three major categories:
Consumers in New England are aggressively migrating away from traditional gelatin, synthetic dyes, and high-fructose corn syrups. Boston brands require pectin-based, sugar-free, vegan gummy delivery formats capable of stabilizing sensitive actives like Chlorophyll, Vegan Omega-3 algal oils, and botanical extracts without structural degradation or moisture migration.
Driven by Boston’s dense workforce of technology and academic professionals, demand for cognitive-enhancing supplements, specialized creatine monohydrate chews, and botanical dandelion 10:1 extract formulations has surged. Toll clients require precise micro-dosing and uniform compression to guarantee potency per serving.
Furthermore, specialized raw materials such as rheology modifiers (Crothix Liquid Thickeners for topical or liquid nutricosmetics) and specialized formulation adjuncts (such as custom optical brightener systems for topical delivery matrices) require advanced blending shear controls that standard supplement re-packers cannot provide. PAG Pharmatech America LLC provides the exact technical capabilities required to process complex multi-phase systems.
Our toll processing factory operates six specialized dosage manufacturing suites. Each line is segregated with dedicated HVAC air handling units (AHUs) to eliminate cross-contamination risks during blending, granulation, compression, and encapsulation.
| Dosage Platform | Standard Tooling / Formats | Toll MOQ Entry | In-Process Quality Controls | Ideal Boston Application |
|---|---|---|---|---|
| Pectin & Gelatin Gummies | Custom Molds, Mogul Depositing, Sugar-Free | 6,000 Units (Bottles) | Brix %, Water Activity (a_w), Active Assay Recovery | Vegan Omega-3, Chlorophyll, Botanical Gummies |
| Custom Powders & Stick Packs | V-Blenders, Augur Filling, Sachet Packets | 300 kg (Bulk Batch) | Bulk Density, Particle Size (Mesh), Homogeneity Analysis | Plant Proteins, Pre-Workout, Electrolyte Blends |
| Tablets & Chewables | Bilayer, Film-Coated, Chewable, Effervescent | 5,000 Units | Hardness (Kp), Friability (<1%), Disintegration Time | Creatine Chews, Nootropic Stack Compression |
| Hard Shell Capsules | HPMC Vegetable, Gelatin (Sizes 000 to 0) | 5,000 Units | Fill Weight Variation (<2%), Tap Density Check | Herbal Extracts (10:1 Dandelion), Nootropic Formulas |
| Softgels | Oval, Oblong, Rotary Die Encapsulation | 5,000 Units | Rupture Time, Seal Integrity, Nitrogen Blanket Fill | High-Potency Lipid Solubles, CoQ10, Algae Oils |
| Pet Nutrition Chews | Cold-Extruded Soft Chews, Functional Powders | 2,000 Units / 300 kg | Palatability Score, Moisture Balance, Mold Inhibitors | Veterinary Supplements, Canine Hip & Joint Chews |
Transferring your custom formulation to our toll manufacturing facility follows a strict 4-stage Quality by Design (QbD) framework. This process ensures that batch-to-batch consistency matches your exact master formula specifications.
Upon receipt of customer-supplied raw materials (such as raw Crothix, botanical powders, or active oils), our Quality Control laboratory performs identity testing via FT-IR, heavy metal screening via ICP-MS, and microbiological plating. Certificates of Analysis (CoA) are verified against your raw material specifications.
Our quality assurance engineers draft a custom MBR detailing step-by-step blending times, impeller speeds, moisture thresholds, drying temperatures, and yield reconciliation targets tailored specifically to your toll run.
A pilot batch is processed to confirm flowability, compressibility, or deposit viscosity. In-process checks monitor weight uniformity, disintegration, hardness, and active ingredient distribution across the blend.
Finished goods undergo final release testing. Each shipment is delivered with a complete Batch Production Record (BPR), Certificate of Analysis (CoA), Allergen Statement, and BSE/TSE declaration ready for immediate retail or Amazon compliance review.
While our primary North American manufacturing infrastructure is rooted in Springville, Utah—offering zero tariff exposure, fast domestic freight routes to Boston logistics hubs, and 8-to-12-week turnarounds—PAG Pharmatech America LLC operates within an integrated international manufacturing network.
Our core US plant. FDA-registered under 21 CFR 111 & 117. Offers high-speed gummy depositing, tablet pressing, capsule filling, and stick-pack filling for North American brands.
Group-owned European facility. Provides Boston brands with a seamless gateway for EU expansion under European Food Safety Authority (EFSA) and Novel Food compliance regulations.
Adds immense raw material sourcing leverage, high-volume secondary production capacity, and R&D backing built upon 30 years of global contract manufacturing heritage.
Key technical and commercial answers for sourcing directors, brand managers, and formulation chemists evaluating toll manufacturing partners.
Whether you require high-shear toll processing for custom botanical powders, pectin gummy depositing, or clinical tablet manufacturing, our technical engineering team is ready to review your Master Formula and project timelines.